01
Function & Material-condition Review
Select the grade for load, temperature, media and moisture together. Define storage, assembly and the moisture condition for dimensional acceptance.
Built for production.
Take your design from tooling to repeat production of custom plastic parts.
Manufacturing Capabilities
Plastic Injection MoldingCustom plastic parts for production Tooling & Design SupportPrepare your part design for tooling High-Volume ProductionPlan repeat runs around your delivery needsMaterials & Finishes
Made for smaller runs.
Produce resin parts with silicone molds for design validation and small batches.
Small-Batch Capabilities
Vacuum CastingResin parts made with silicone moldsLow-Volume ProductionFrom trial parts to small-batch deliveryAppearance & Fit ChecksPrepare multiple parts for product checksMaterials & Finishes
Other Services
Machining, printing, and supporting services for specific part needs.
Materials & Finishes
Explore material performance and appearance options separately.
Explore Materials & Finishes
Injection Molding Materials
Choose molding materials for strength, heat resistance and appearance.
Manufacturing Knowledge
Find articles, answers, and case studies to help prepare your project.
Start with your part requirements.
Contact PlasticHubs for help with quotes, files, delivery, and orders.
Files, Orders & Delivery
Industries
Explore manufacturing options for your product application.
Start with your manufacturing needs
From tooling to production of plastic parts.
Small batches of resin parts made with silicone molds.
Start with your design, material, and quantity.
Plan PPA injection molding for equipment parts that need elevated-temperature stiffness, chemical compatibility and stable fit. Review the polyamide formulation, reinforcement direction and moisture condition, then connect drying, tooling and actual-sample validation.
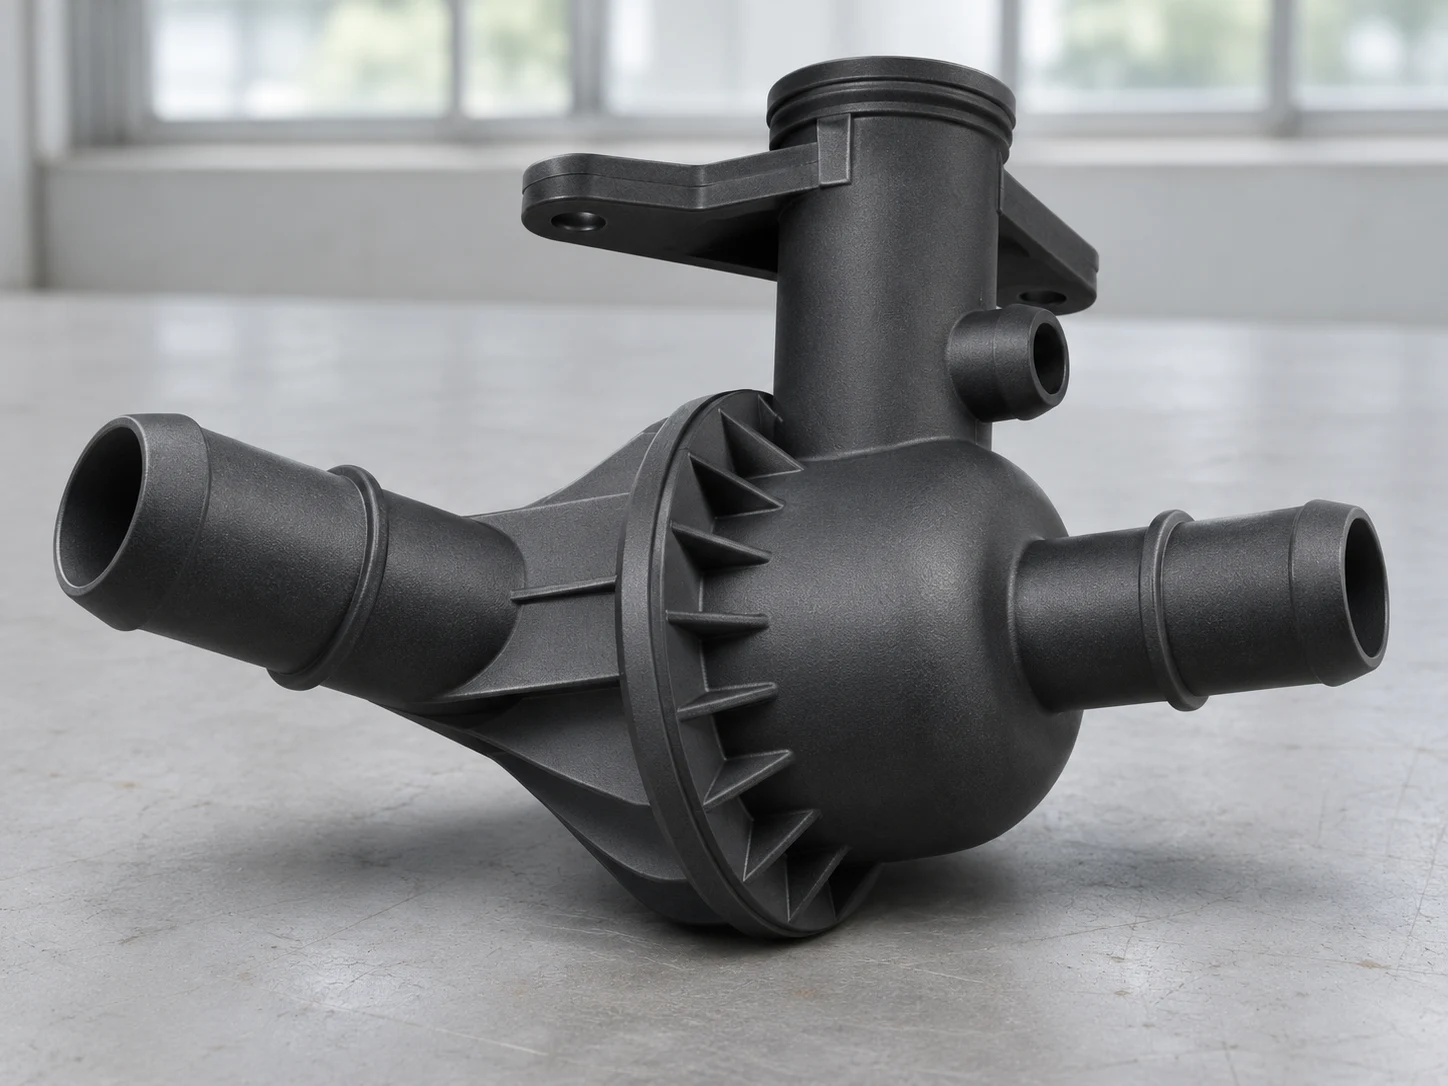
Describe temperature, chemical exposure and loading, and whether dimensions are accepted dry or after conditioning. Identify critical assembly, sealing or electrical interfaces to establish the grade and molding approach.
Discuss your project ↗Select the grade for load, temperature, media and moisture together. Define storage, assembly and the moisture condition for dimensional acceptance.
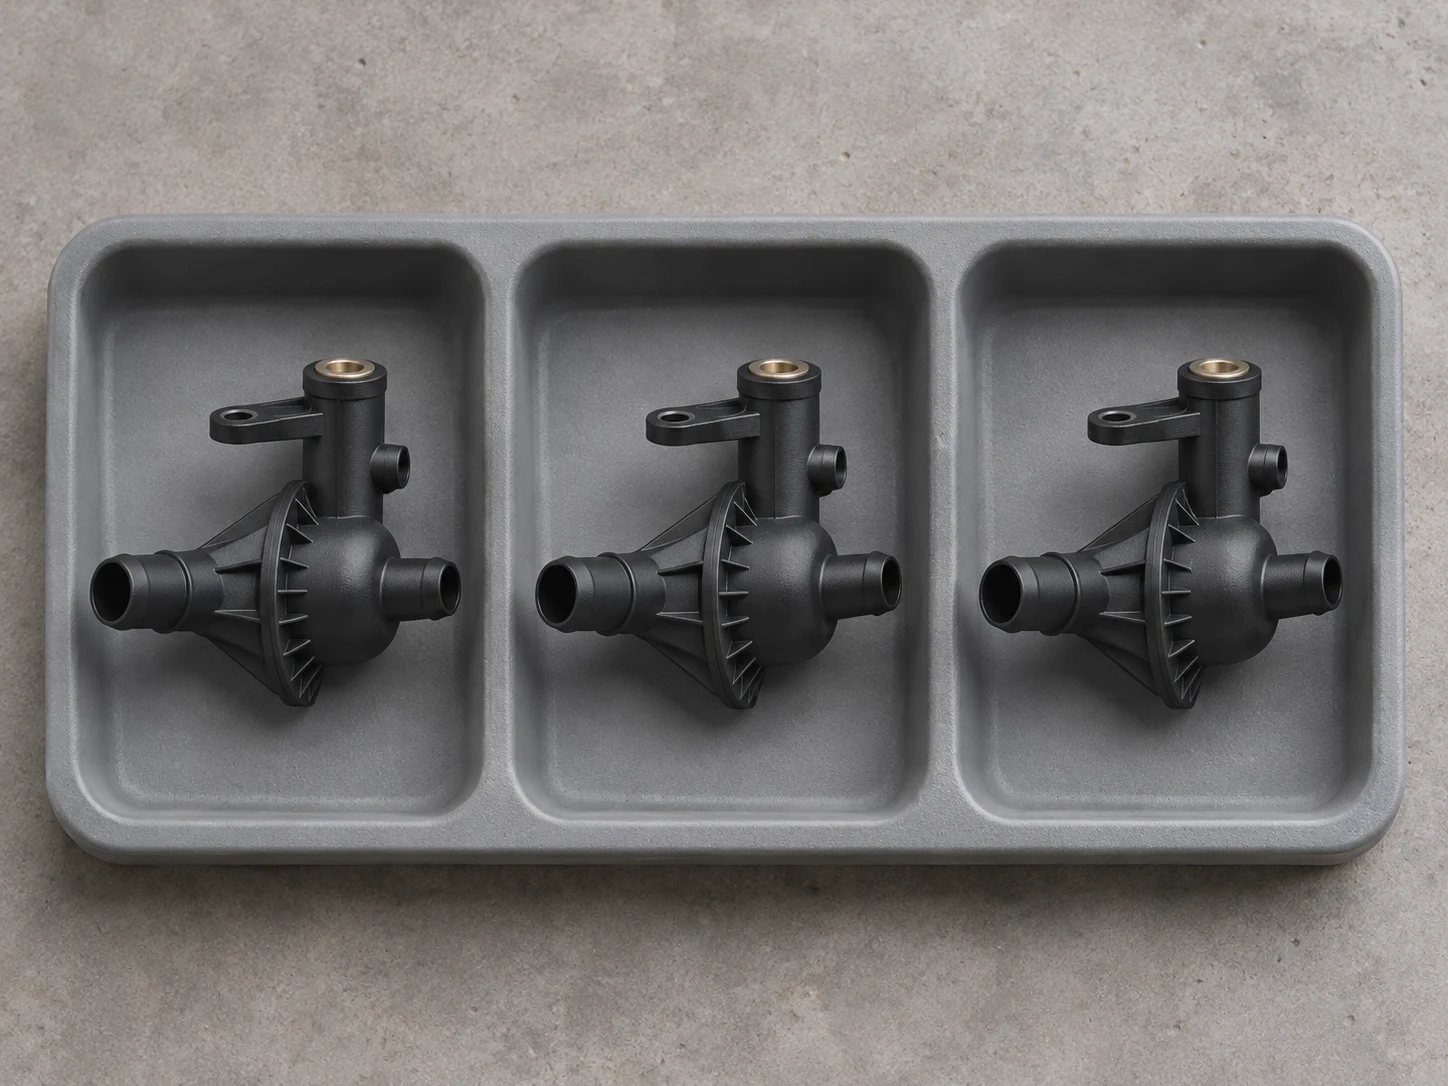
Prepare material to grade guidance, reviewing melt heat history, mold temperature, flow and cooling. Use samples and relevant tests to establish the production baseline while managing moisture reabsorption and process variation.
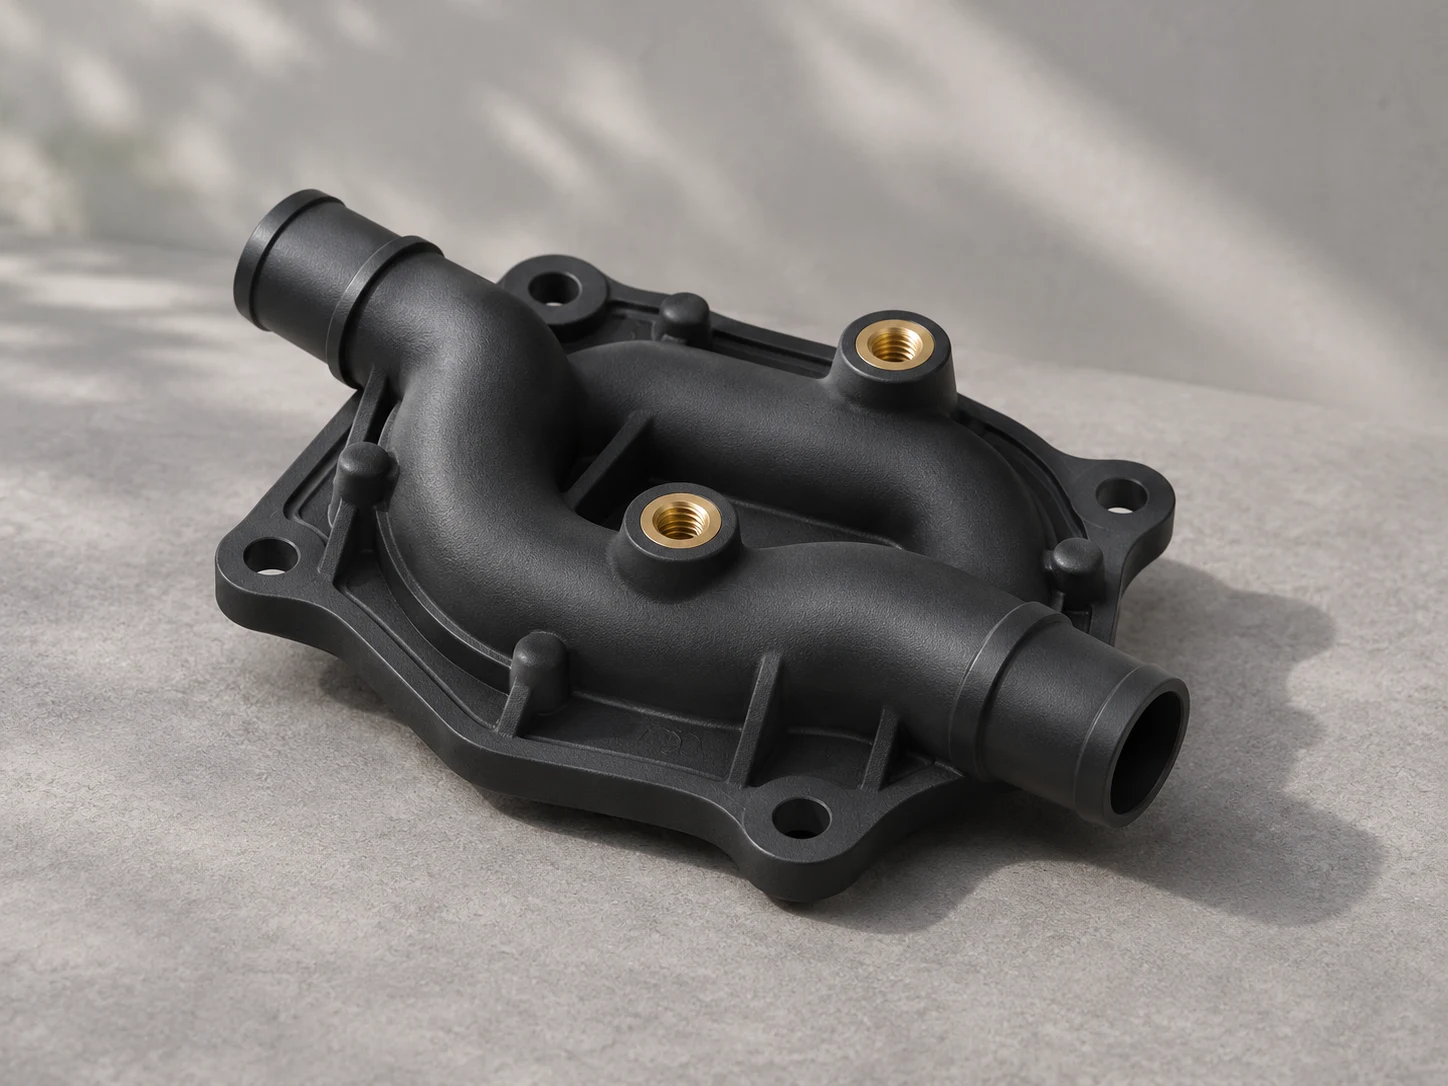
Compare directionality, sections, fit and local loading when selecting reinforced or specialty formulations. Connect actual geometry, material condition and sample inspection to establish the project specification.
Share drawings, quantity, temperature, media and material-condition requirements.
| Project focus | Review scope |
|---|---|
| Grade and operating conditions | Confirm the PPA formulation, reinforcement, media, temperature and loading, using data for the exact grade and material condition. |
| Drying and material handling | Use grade guidance for predrying, allowed moisture and storage/transfer to manage reabsorption after drying. |
| Tooling, flow and thermal control | Review gates, vents, fiber direction, balanced cooling and melt dwell together. |
| Dimensions and conditioning state | Define mating, sealing and locating dimensions from drawings, specifying material condition during measurement and acceptance. |
| Samples and functional checks | Plan loaded chemical-exposure, thermal-cycle, humidity and electrical tests for the project, recording dimensional and functional results separately. |

Use smooth section transitions and reduce heavy intersections and sharp corners. Review local stress and notch effects around slender fingers, clips and loaded regions, confirming toughness with samples of the selected grade.
Coordinate flow paths around critical fits, accounting for shrinkage and loading differences from fiber direction. Review weak weld lines and unbalanced filling early in the design.
Provide venting, cooling and ejection support around deep ribs, long flow paths and slender cores. Temperature distribution and release affect warpage and residual stress; verify them together in trials.
Record material condition from drying/transfer through measurement and assembly. Reinforced PPA dimensions and properties can still change with moisture, requiring consistent acceptance conditions.
Define surfaces against mating, contact, cleaning and appearance requirements. Formulation, drying and molded condition affect results, confirmed through actual samples and acceptance conditions.

Mark visible faces, assembly contacts and acceptance areas on the drawing. Review flow direction, gate and parting-line placement, and surface texture on molded samples of the selected PPA.
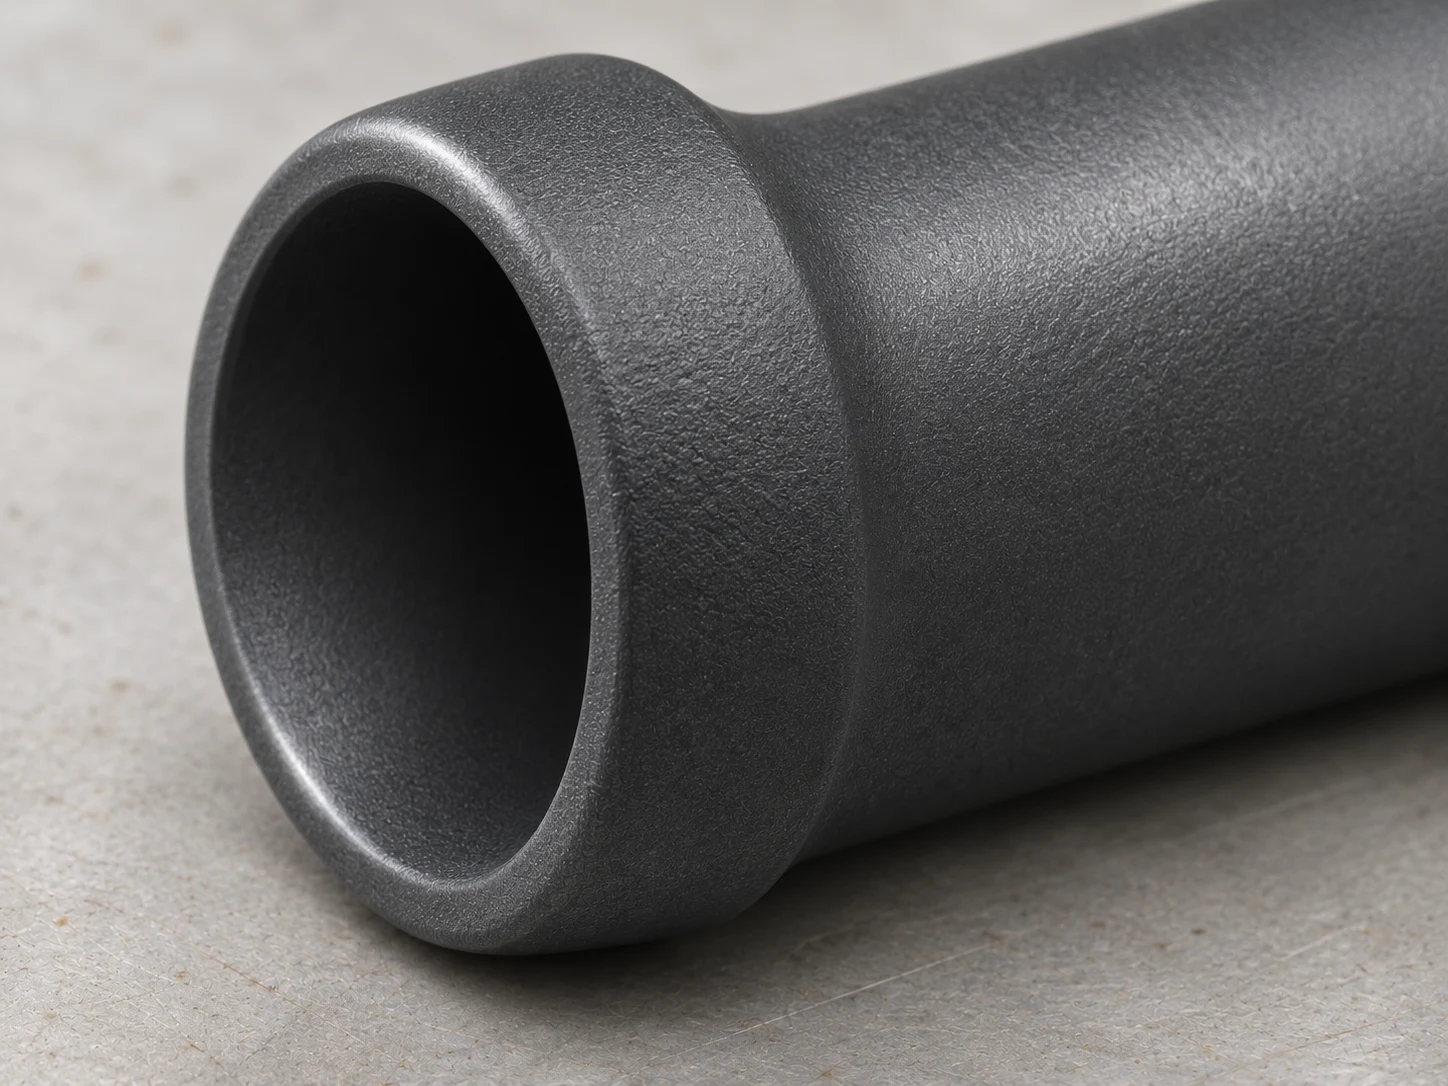
Select tool polish for geometry, appearance and release. Use a finish sample to communicate the target and check replication in the selected PPA formulation.

Review texture placement with draft, fit and contact requirements. Reinforcement direction and molded condition can affect appearance, requiring defined samples and acceptance locations.
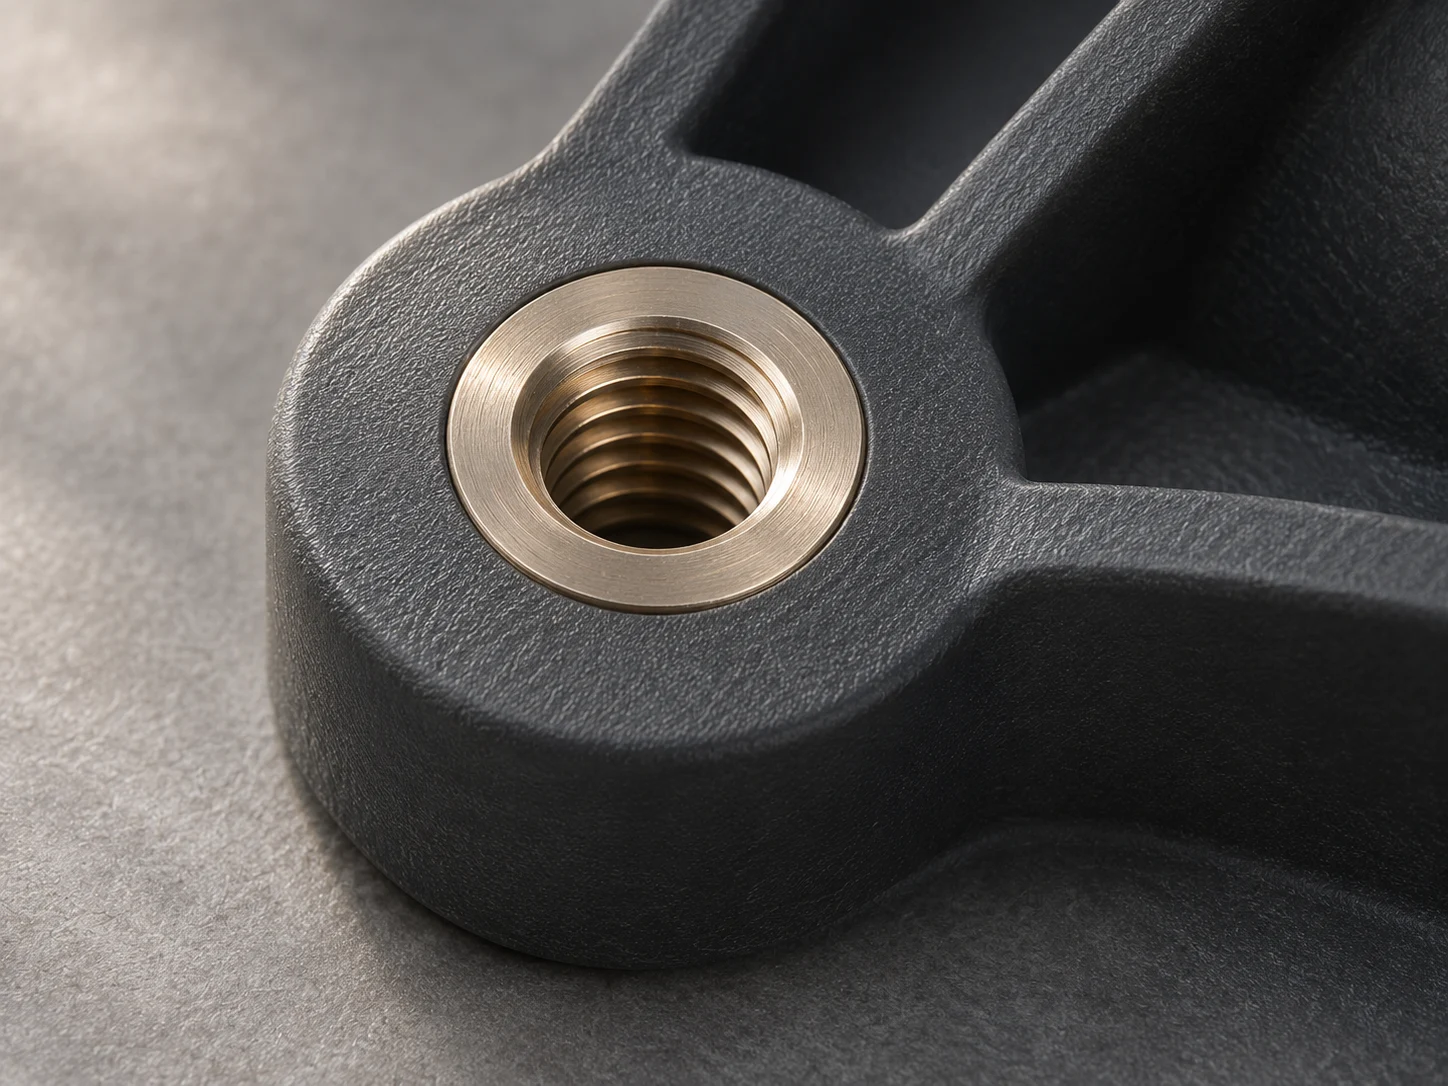
Define datums, fits and assembly acceptance around openings, locating and connection faces. Review samples under consistent moisture and measurement conditions, assessing any secondary operations for the project.
Record the grade, batch, drying and conditioning state with critical dimensions. Test parts under the combination of heat, chemicals, humidity and loading expected in service.
The table uses BASF CAMPUS data for Ultramid Advanced N3HG6 UN, PA9T-GF30. Paired values are shown dry first and conditioned second. Compare grades and formulations under the moisture state used for acceptance.
| Property | Reference value | Method / condition |
|---|---|---|
| Density | 1370 kg/m³ | ISO 1183; dry, conditioned value not listed |
| Tensile modulus: dry / conditioned | 10500 / 10000 MPa | ISO 527; dry / cond |
| Stress at break: dry / conditioned | 190 / 150 MPa | ISO 527; dry / cond |
| Strain at break: dry / conditioned | 2.5 / 1.8% | ISO 527; dry / cond |
| Notched Charpy impact strength | 9 kJ/m² | ISO 179/1eA; +23°C; dry, conditioned value not listed |
| Melting temperature | 300°C | ISO 11357-1/-3; 10°C/min; dry |
| Temperature of deflection under load | 270°C | ISO 75-1/-2; 1.80 MPa; dry |
| Item | Guidance / reference | Method / conditions |
|---|---|---|
| Predrying temperature and time | 120°C / 8 h | Producer preprocessing guidance |
| Maximum allowed water content | 0.05% | Maximum in the producer Pre/Post-processing entry |
| Melt-temperature range | 320–340°C | Official injection range; recommended point 330°C is listed separately |
| Mold-temperature range | 125–160°C | Official injection range; recommended point 140°C is listed separately |
| Melt dwell time | 5 min | Producer thermoplastics dwell-time entry; not the part cycle time or an invented maximum |
| Molding shrinkage: parallel / normal | 0.47% / 0.98% | ISO 294-4, 2577; both dry, conditioned values not listed |
For ISO 294 specimen preparation, BASF lists a 330°C melt and a 140°C mold. The five-minute dwell is a processing condition. Use the injection ranges to plan trials and define the moisture and measurement conditions for part acceptance.
Reference: BASF-published CAMPUS Ultramid Advanced N3HG6 UN datasheet, hosted by Altair; actually read October 21, 2026. No grade-revision date is shown in the capture.
Review dry/conditioned state and grade selection alongside temperature, chemical exposure and assembly requirements.
Connect drying, reinforcement direction, mold temperature and critical dimensions in a clear trial and acceptance plan.
Use drawings and dimensional inspection support, including CMM, to focus on location, fit and measurement conditions; test relevant functions for the project.
Use ISO 9001 / ISO 13485 quality systems and material, sample and inspection records to support development through production.
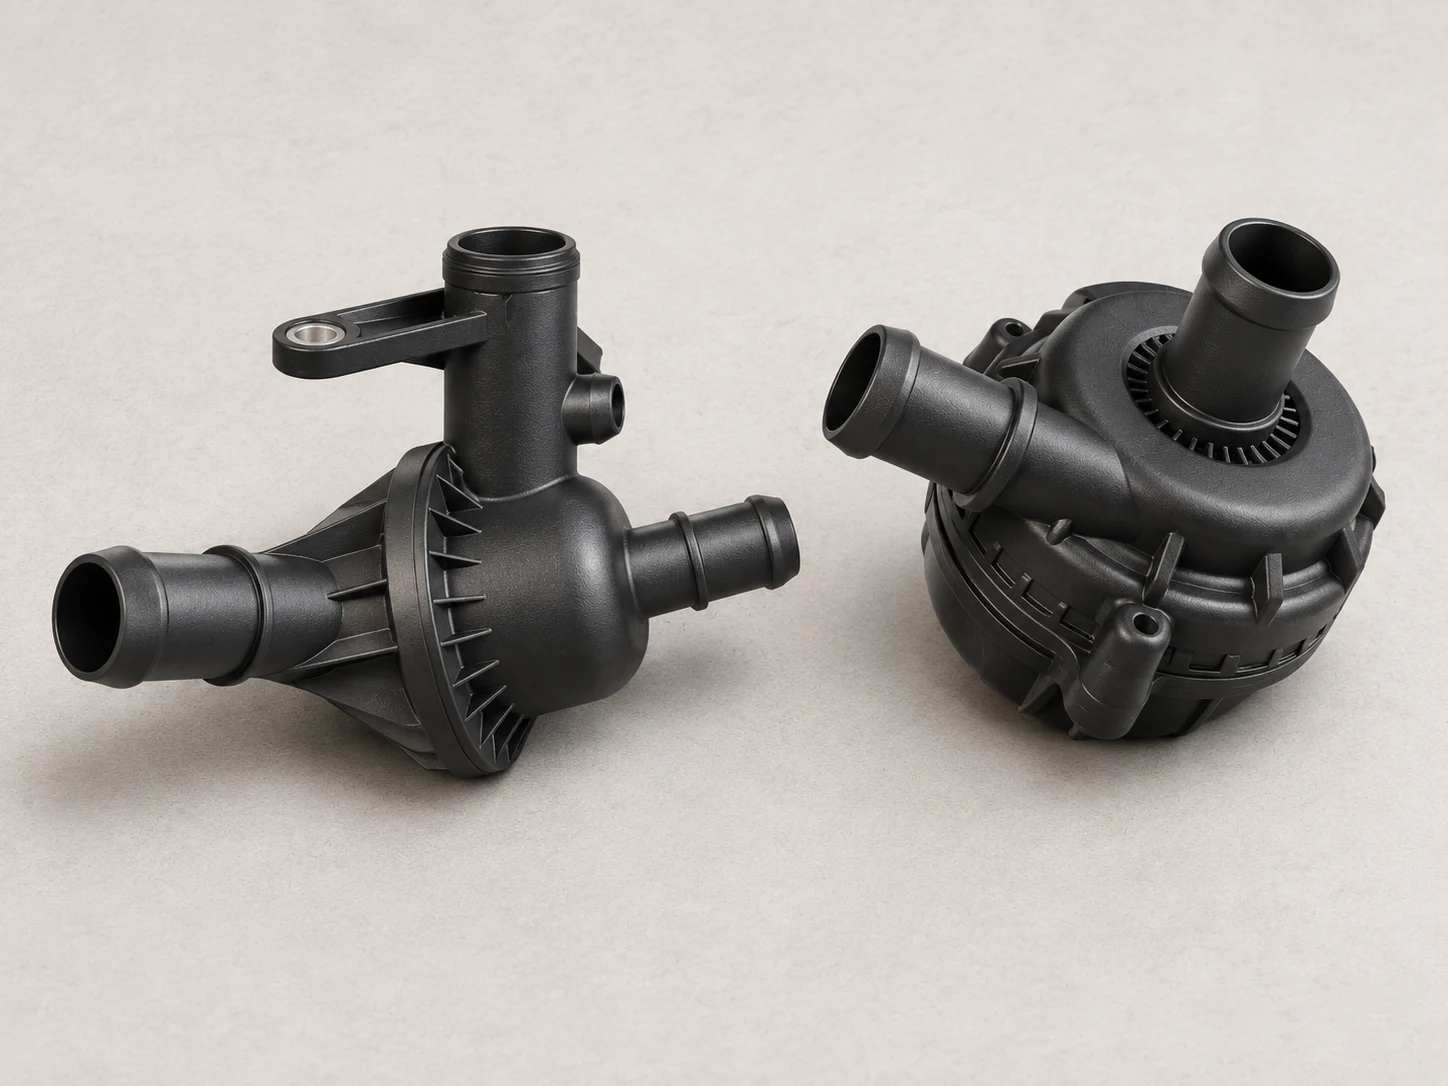
PPA, polyphthalamide, is a family of semi-aromatic high-performance polyamides, often glass- or mineral-reinforced for elevated-temperature stiffness and dimensional requirements. Polyamide structures and filler systems differ in moisture, thermal and mechanical behavior; the PPA name alone does not define performance.
The N3HG6 UN reference grade is PA9T-GF30. Moisture still affects material condition, requiring consistent preparation, molding and dimensional/functional validation. For coolant, fuel or electrical interfaces, establish compatibility and acceptance against the formulation and actual exposure.
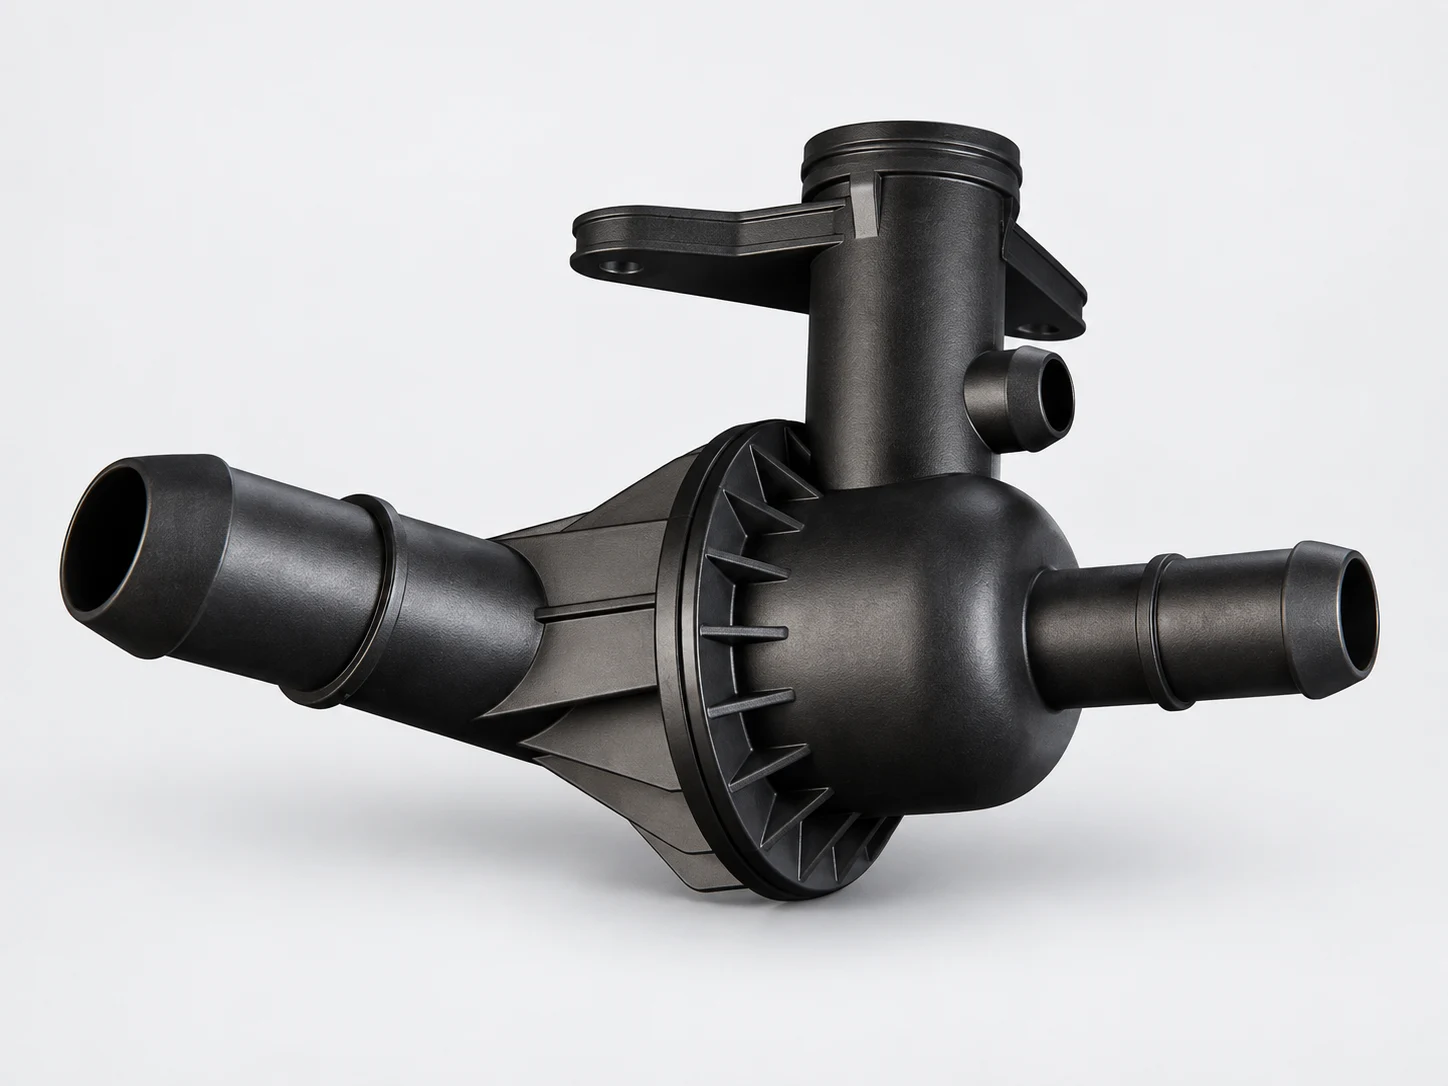
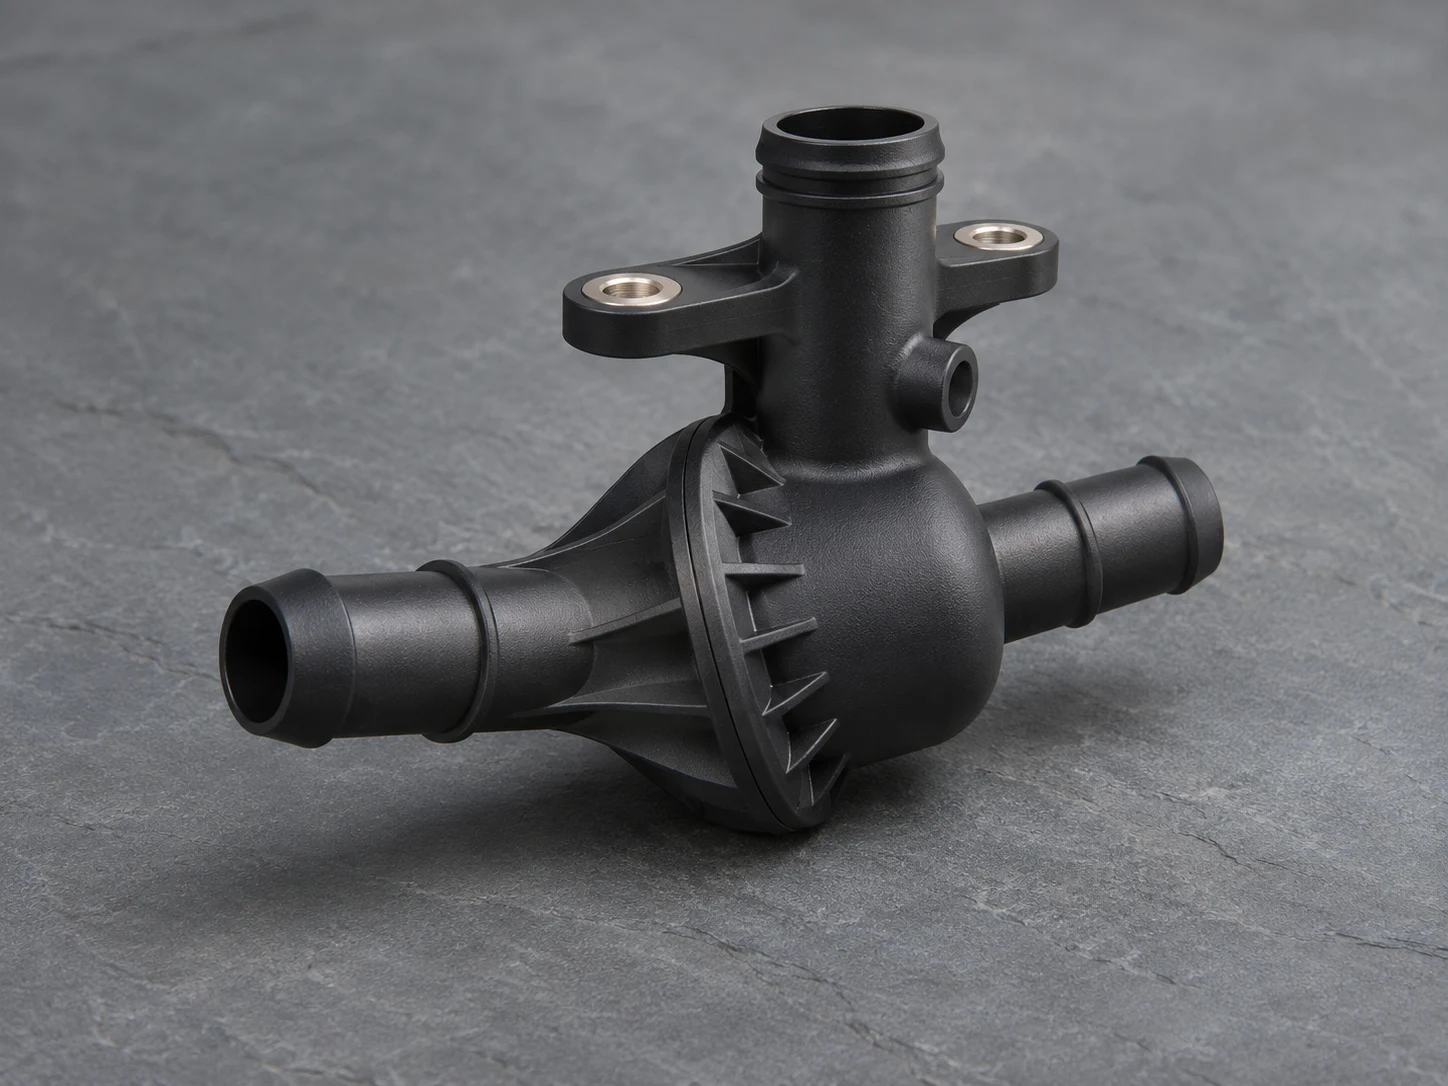
Review assembly space, connection method and sealing interfaces around multi-directional ports. Select the PPA grade for actual coolant, temperature, pressure and loading, confirming connection regions through samples and cycle tests.

For multiple openings and inserts, define locating, connections, adjacent materials and local loading. Review wall transitions, reinforcement direction and dimensional condition against the drawing, then confirm insert retention and sealing requirements.
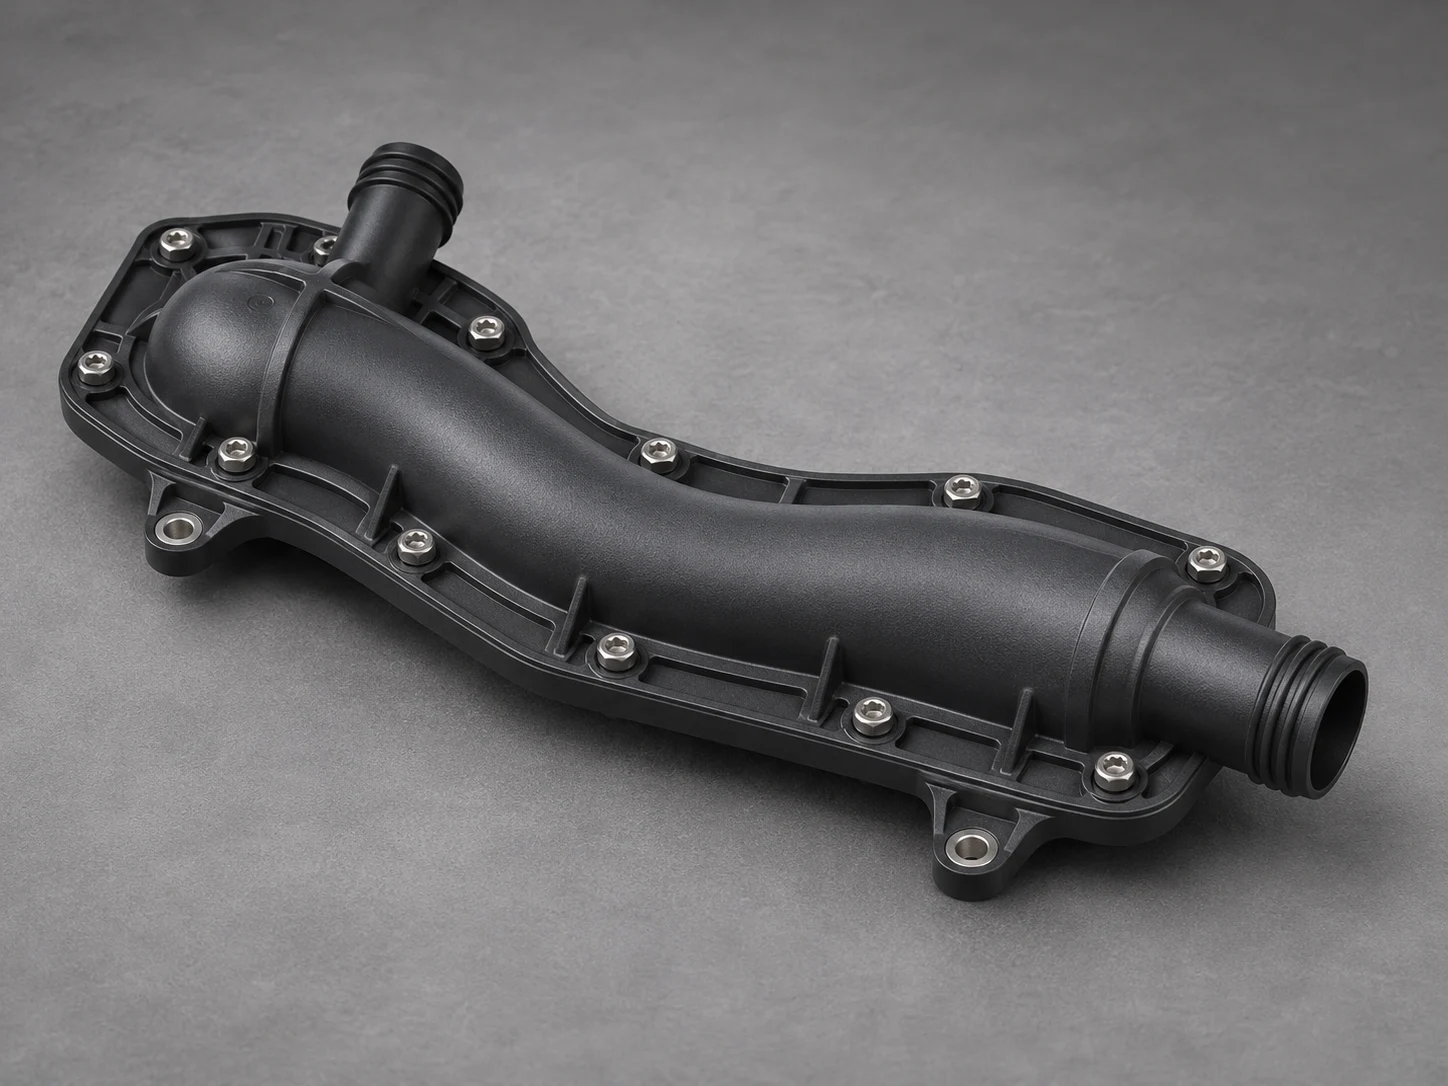
Coordinate filling, venting, cooling and release support around long channels and flanges. Review shrinkage, warpage and connection-face dimensions against flow and fiber direction, accepting samples under a specified moisture condition.
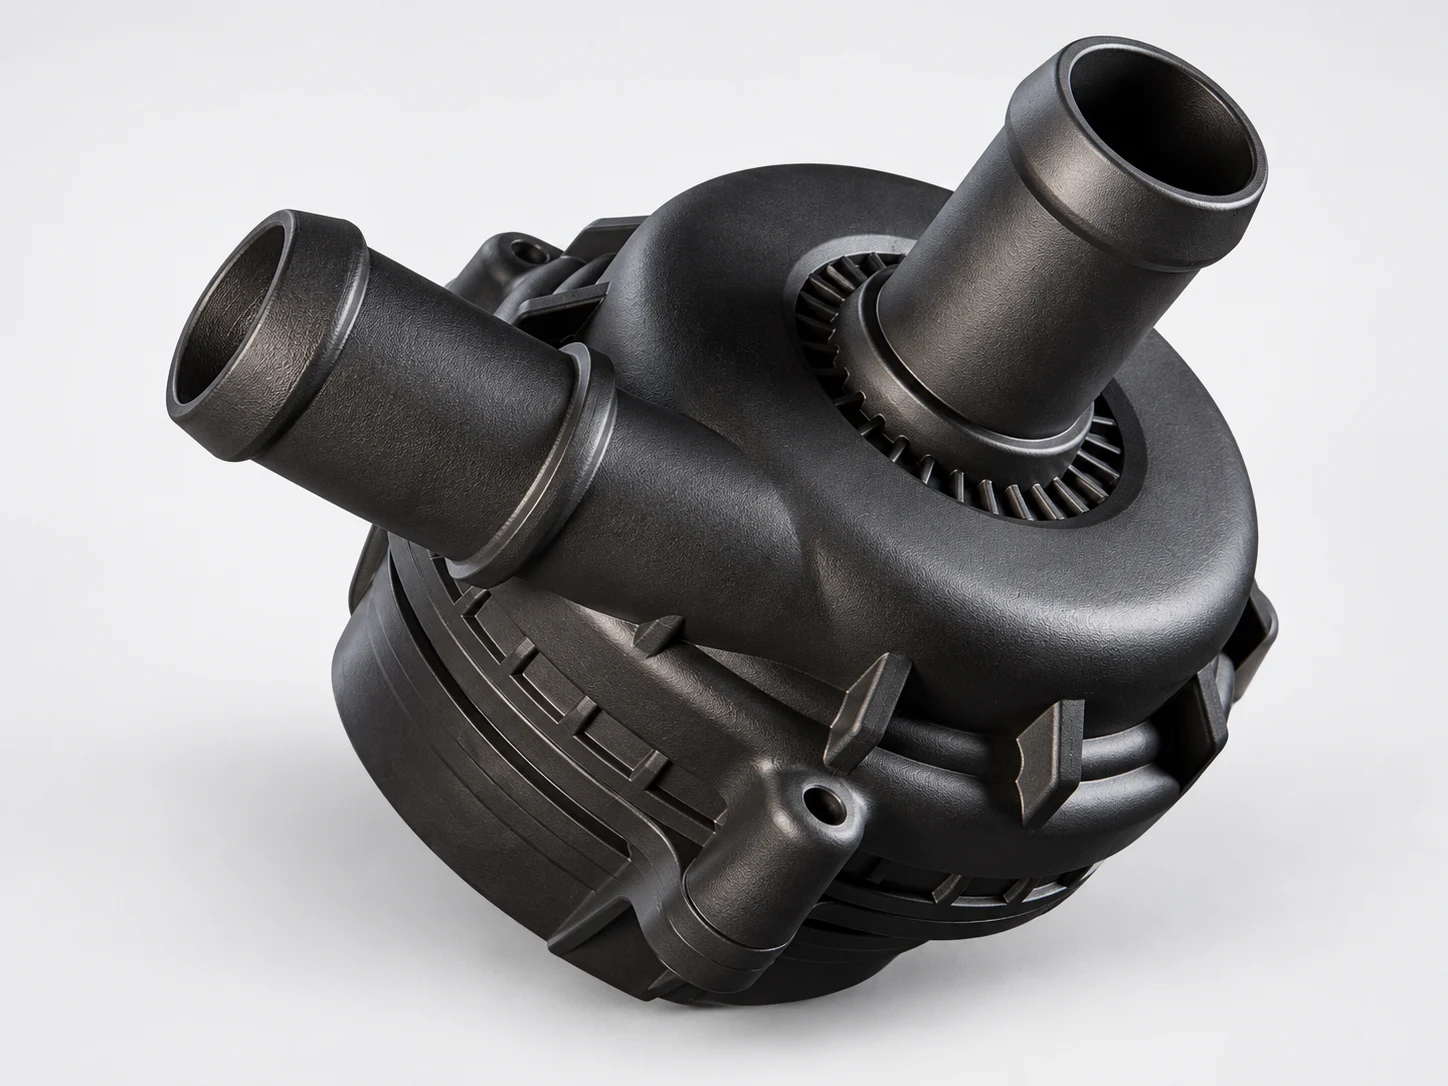
Review angled ports, ribs and mounting regions with neighboring components. Specify locating dimensions, clearances and contact surfaces, and check fit at the intended temperature and chemical exposure.
Consider a specific PPA formulation where conventional polyamides do not meet thermal, loading or dimensional tasks. Compare dry and conditioned behavior, then assess geometry and actual exposure.
Drying equipment, material transfer, thermal tooling and trial validation all affect investment. Include quantity, geometry, dimensional condition and functional needs in the quote rather than deciding by resin price alone.
PPA INJECTION MOLDING FAQ
Common questions about grades, moisture condition, processing and project validation.
PPA belongs to the semi-aromatic polyamide family and is often selected for stiffness and dimensional needs at elevated temperature. It includes different polymer structures and reinforcement systems. The PA9T-GF30 reference here is one grade, not every PPA.
No. N3HG6 UN lists tensile modulus of 10500 MPa dry and 10000 MPa conditioned, with stress at break of 190 / 150 MPa. Compare dimensions, loading and acceptance under consistent conditions; do not infer unlisted conditioned values.
N3HG6 UN calls for predrying at 120°C for 8 hours and a maximum allowed water content of 0.05%. Use the selected grade’s values for drying and control moisture during transfer and storage.
N3HG6 UN lists dry melting temperature at 300°C and HDT at 270°C under 1.80 MPa. Its injection melt range is 320–340°C and mold range is 125–160°C. Set prolonged service conditions from the actual load, temperature and exposure.
Specific formulations serve relevant applications, but suitability depends on chemical, concentration, temperature, duration and load. Family-level chemical-resistance descriptions do not replace grade records and component tests, particularly for acids or alkalis.
Specify the dry or conditioned measurement state, critical datums and target tolerances. Review reinforcement direction and shrinkage during trials, then set acceptance using molded samples and the agreed inspection method.
For N3HG6 UN, the listed IEC 60695-11-10 result is HB at 0.8 mm. If your part calls for V-0, specify the required test, color and thickness so an appropriate documented grade can be selected.
Share drawings, quantity, temperature, media and material-condition requirements. Our team will review the material and manufacturing route and prepare a quote.
Get a PPA Molding Quote