01
Development & Interface Review
Review walls, radii, draft and critical fits before tooling. Use machined samples for geometry and assembly, and molded samples to evaluate residual stress, flow marks and shrinkage.
Built for production.
Take your design from tooling to repeat production of custom plastic parts.
Manufacturing Capabilities
Plastic Injection MoldingCustom plastic parts for production Tooling & Design SupportPrepare your part design for tooling High-Volume ProductionPlan repeat runs around your delivery needsMaterials & Finishes
Made for smaller runs.
Produce resin parts with silicone molds for design validation and small batches.
Small-Batch Capabilities
Vacuum CastingResin parts made with silicone moldsLow-Volume ProductionFrom trial parts to small-batch deliveryAppearance & Fit ChecksPrepare multiple parts for product checksMaterials & Finishes
Other Services
Machining, printing, and supporting services for specific part needs.
Materials & Finishes
Explore material performance and appearance options separately.
Explore Materials & Finishes
Injection Molding Materials
Choose molding materials for strength, heat resistance and appearance.
Manufacturing Knowledge
Find articles, answers, and case studies to help prepare your project.
Start with your part requirements.
Contact PlasticHubs for help with quotes, files, delivery, and orders.
Files, Orders & Delivery
Industries
Explore manufacturing options for your product application.
Start with your manufacturing needs
From tooling to production of plastic parts.
Small batches of resin parts made with silicone molds.
Start with your design, material, and quantity.
Plan PEI molding for equipment components that combine heat resistance, stiffness and electrical insulation. Define grade, chemical exposure and assembly requirements, then connect drying, high-temperature processing and critical-interface checks with the project.
Identify dimensions that control fit, electrical separation or sealing, and describe temperature, load, cleaning agents and cycling. Select the PEI grade and tooling against the operating environment, quantity and validation work.
Discuss your project ↗Review walls, radii, draft and critical fits before tooling. Use machined samples for geometry and assembly, and molded samples to evaluate residual stress, flow marks and shrinkage.
Connect resin drying, melt heat history, filling/packing and cooling. Establish the acceptable condition through samples and relevant tests before defining the production baseline.
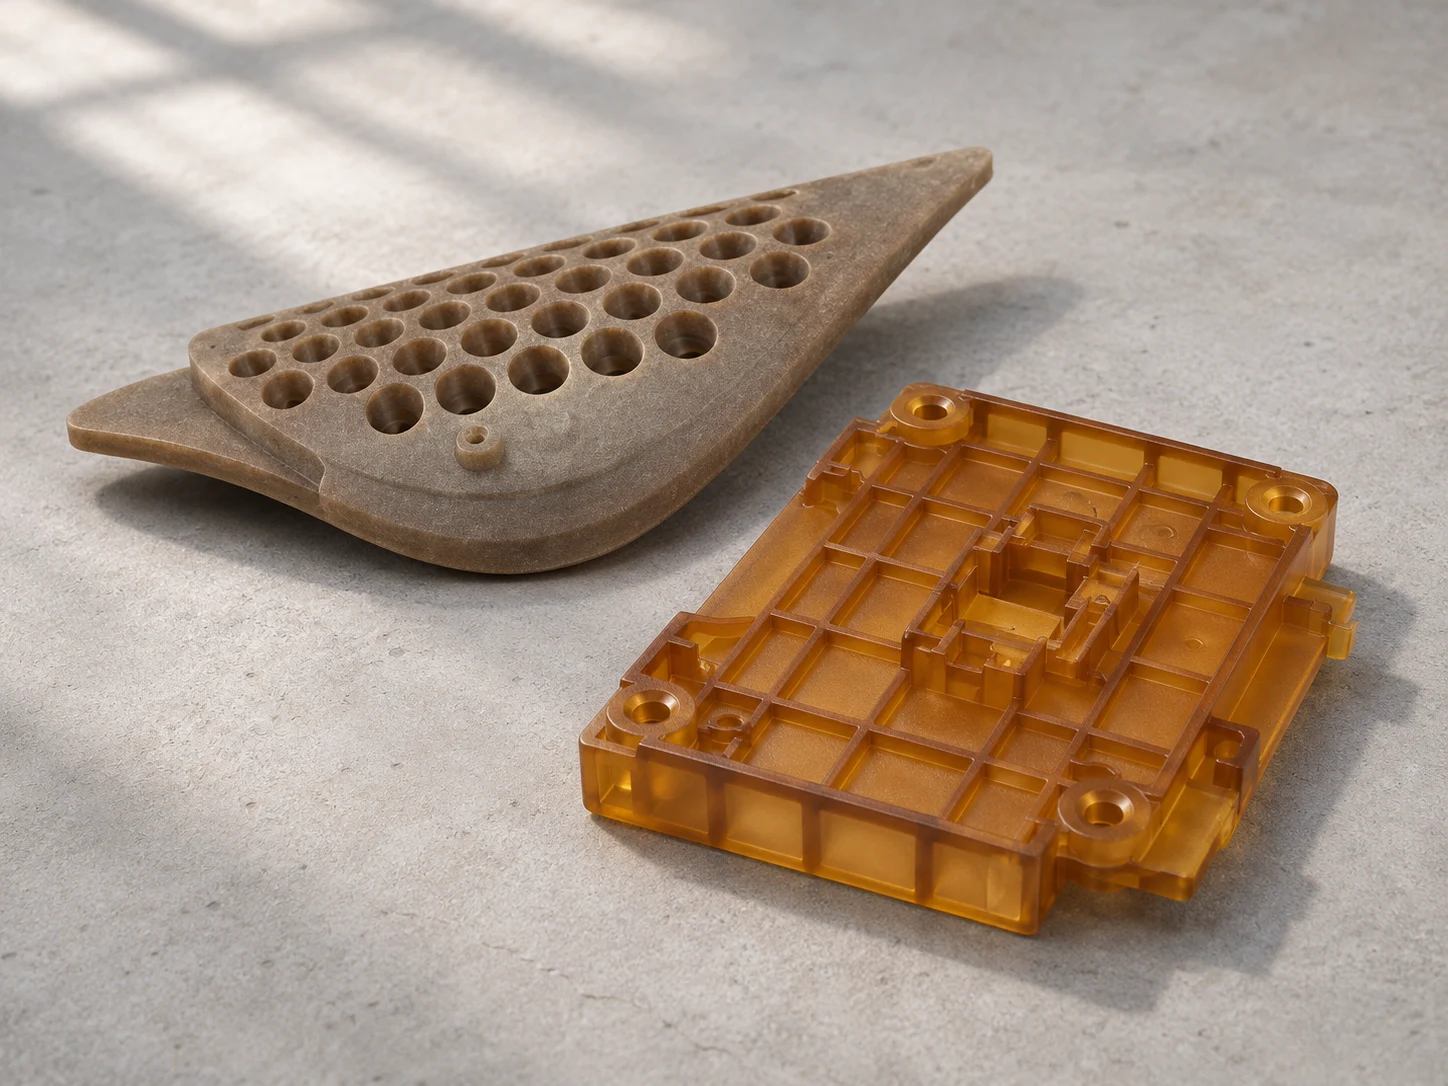
Unfilled, glass-reinforced and healthcare formulations have different records and performance limits. Select for stiffness, insulation, color, cleaning and directional behavior rather than the ULTEM name alone.
Share drawings, quantity and thermal, electrical or cleaning requirements.
| Project focus | Review scope |
|---|---|
| Grade and operating environment | Confirm reinforcement, color, temperature, chemical exposure and material records; do not transfer values across grades. |
| Drying and melt heat history | Use grade guidance for moisture and drying, reviewing high-temperature residence, changeover and material-path cleanliness. |
| Tooling and molding | Evaluate flow, vents, gates, packing and cooling together, focusing on heavy sections, weld lines and residual stress. |
| Critical interfaces | Define assembly, sealing and electrical dimensions from drawings; establish tolerances against orientation, measurement conditions and approved samples. |
| Samples and acceptance | Separate appearance, dimensional, load, electrical and cleaning-cycle tests, selecting the checks required for the project. |

Use smooth section transitions and reduce sharp corners and heavy intersections. Review filling, cooling, sink and internal-void risks in thick sections.
Coordinate gate location, flow direction and packing around critical fits. For reinforced grades, review fiber orientation and its effect on shrinkage, dimensions and loading.
Provide suitable vents and draft around deep ribs, long flow paths and textured faces. Apply ejection force to supported regions to limit release distortion and concentrated stress.
Review residual stress where loads, cleaning agents or thermal cycling occur. PEI is amorphous and does not use PEEK crystallinity-control rules; validate with actual samples.
Define contact, assembly, cleaning and visible surfaces. Specify the exact PEI grade and color, then review material documentation against the intended use.
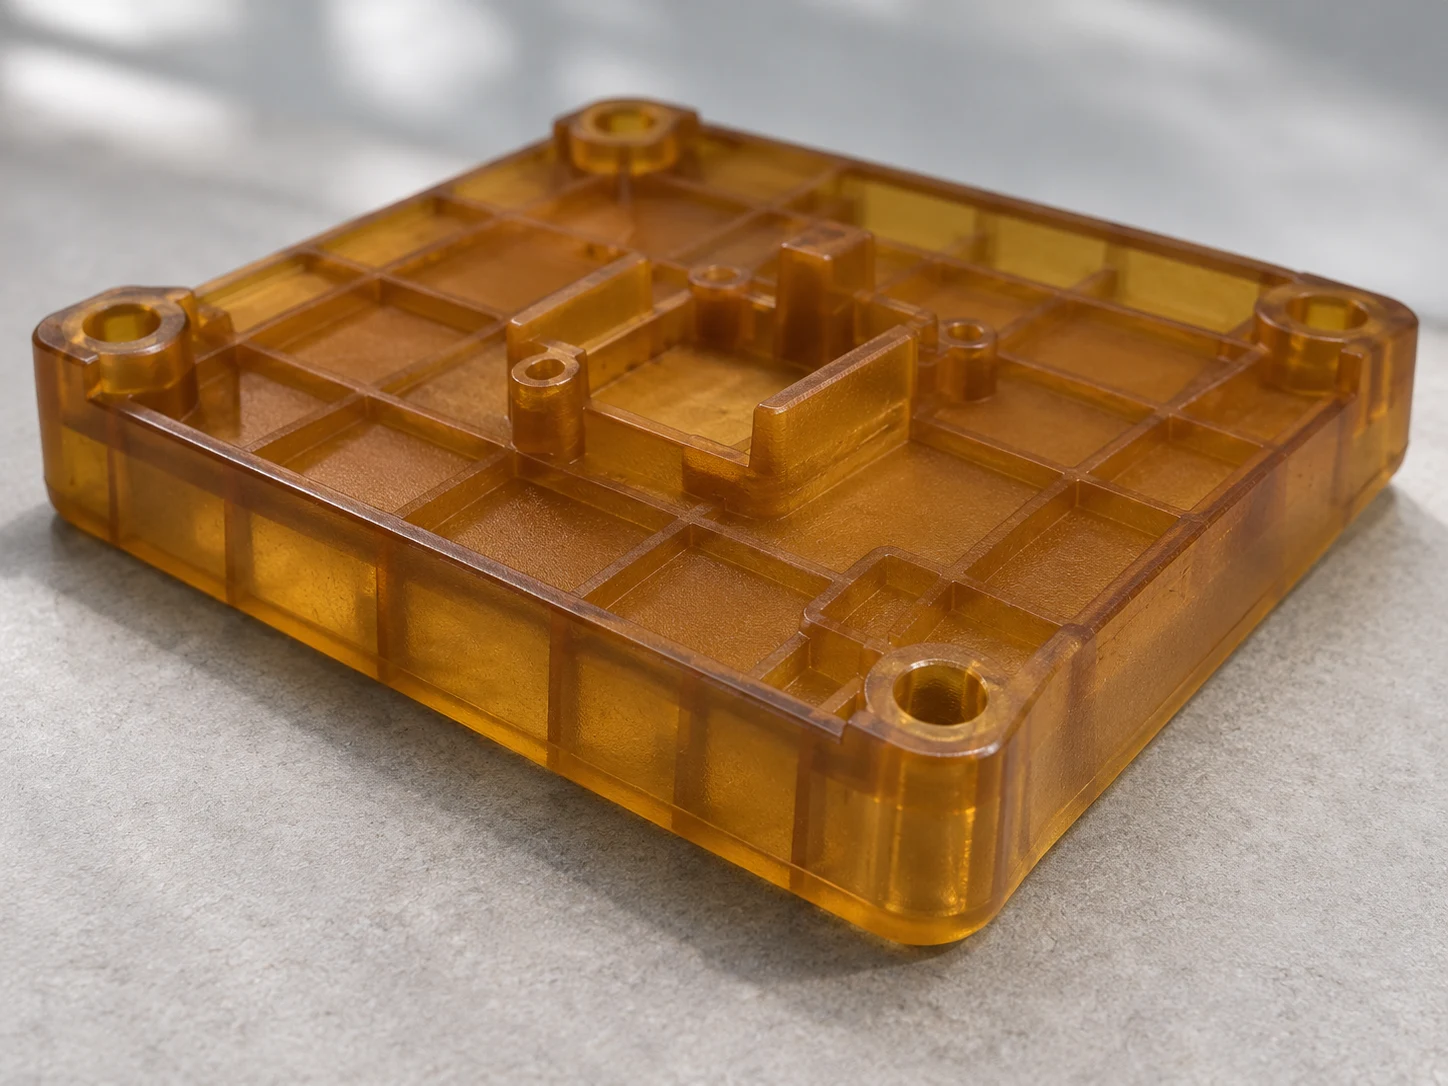
Mark visible faces, openings, mounts and contact locations on the drawing. Agree on finish, surface roughness where relevant and assembly fit using molded samples of the selected PEI.

Use tool-polish samples to set surface targets alongside release and geometry. Check clarity, gloss and visible defects on molded samples for transparent formulations.
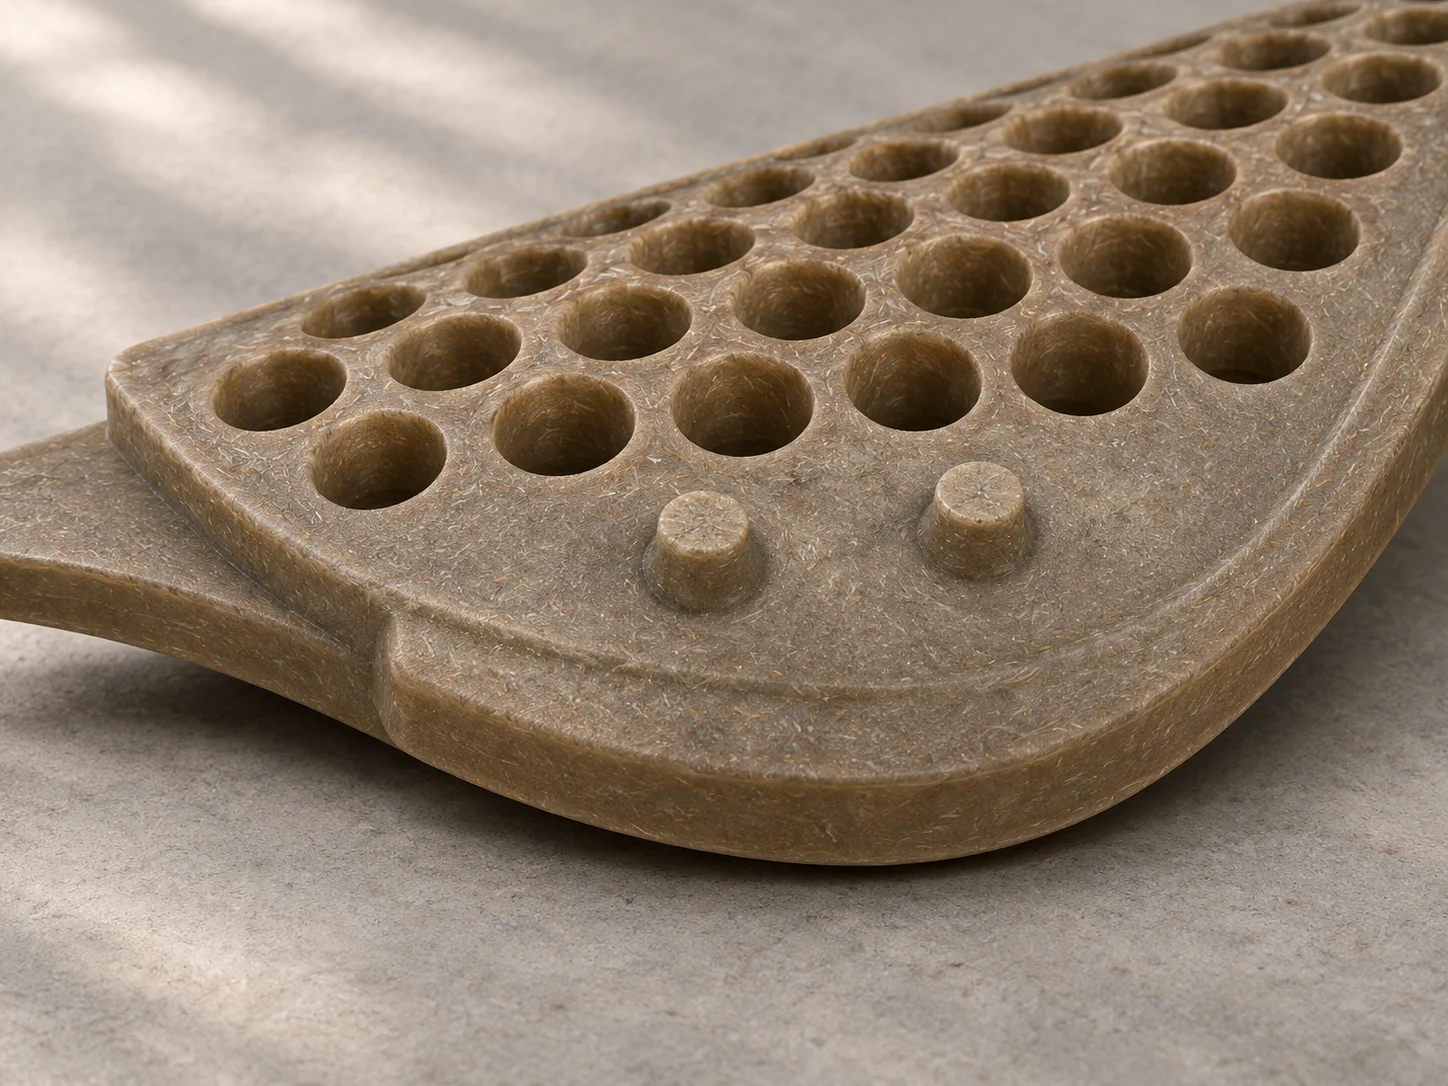
Review texture placement against mating or electrical interfaces, cleaning needs and draft. Confirm replication against the selected grade, tool surface and molded samples.

Define fits and datums around openings, connectors and locating faces. Check the actual assembly and assess post-mold machining for faces that need tighter location or fit.
Record the grade, color, batch and critical dimensions with the samples. Specify component-level tests for electrical strength, chemical exposure under load and cleaning cycles, plus any device-level requirements.
This table uses SABIC’s Europe-region data for unreinforced ULTEM 1000. Compare candidate formulations using the matching test method, specimen and service conditions.
| Property | Typical value | Method / conditions |
|---|---|---|
| Density | 1.27 g/cm³ | ISO 1183 |
| Tensile stress at yield | 110 MPa | ISO 527; 50 mm/min |
| Tensile modulus | 3200 MPa | ISO 527; 1 mm/min |
| Flexural modulus | 3300 MPa | ISO 178; 2 mm/min |
| Notched Izod impact strength | 6 kJ/m² | ISO 180/1A; +23°C; 80 × 10 × 4 mm |
| Heat deflection temperature, HDT/Af | 192°C | ISO 75/Af; 1.8 MPa; flatwise80 × 10 × 4 mm specimen, 64 mm span |
| Dielectric strength in air | 32.7 kV/mm | ASTM D149; 1.6 mm |
| Item | Value | Method / conditions |
|---|---|---|
| Drying temperature and time | 150°C / 4–6 h | Official injection-molding guidance; not extrusion conditions |
| Maximum moisture content | 0.02% | Maximum value in official injection-molding guidance |
| Melt temperature | 350–410°C | Official injection-molding guidance; not glass-transition or service temperature |
| Mold temperature | 135–180°C | Official injection-molding guidance; adjust and confirm for the project |
| Mold shrinkage: flow | 0.5–0.7% | SABIC method; 3.2 mm laboratory coupon; see limitations below |
| Mold shrinkage: across flow | 0.5–0.7% | SABIC method; 3.2 mm laboratory coupon; see limitations below |
Use SABIC’s injection ranges to plan trials for the geometry, shot size and equipment. The shrinkage results come from test coupons. Study shrinkage in the intended tool and compare thermal and electrical results using the listed test methods and specimen sizes.
Reference: official SABIC ULTEM 1000 Technical data, Europe, Revision 25/06/2026; actually expanded and read October 21, 2026.
Review PEI grades against heat, insulation, fit and cleaning requirements, bringing key risks into quoting and development.
Use one project baseline for drying, molding heat history, critical dimensions and relevant tests to reduce handoff gaps.
Use drawings and dimensional inspection support, including CMM, to focus on location and fit; confirm electrical, cleaning or load-related function through relevant tests.
Use ISO 9001 / ISO 13485 quality systems and clear material, sample and inspection records to support the transition from development to ongoing production.
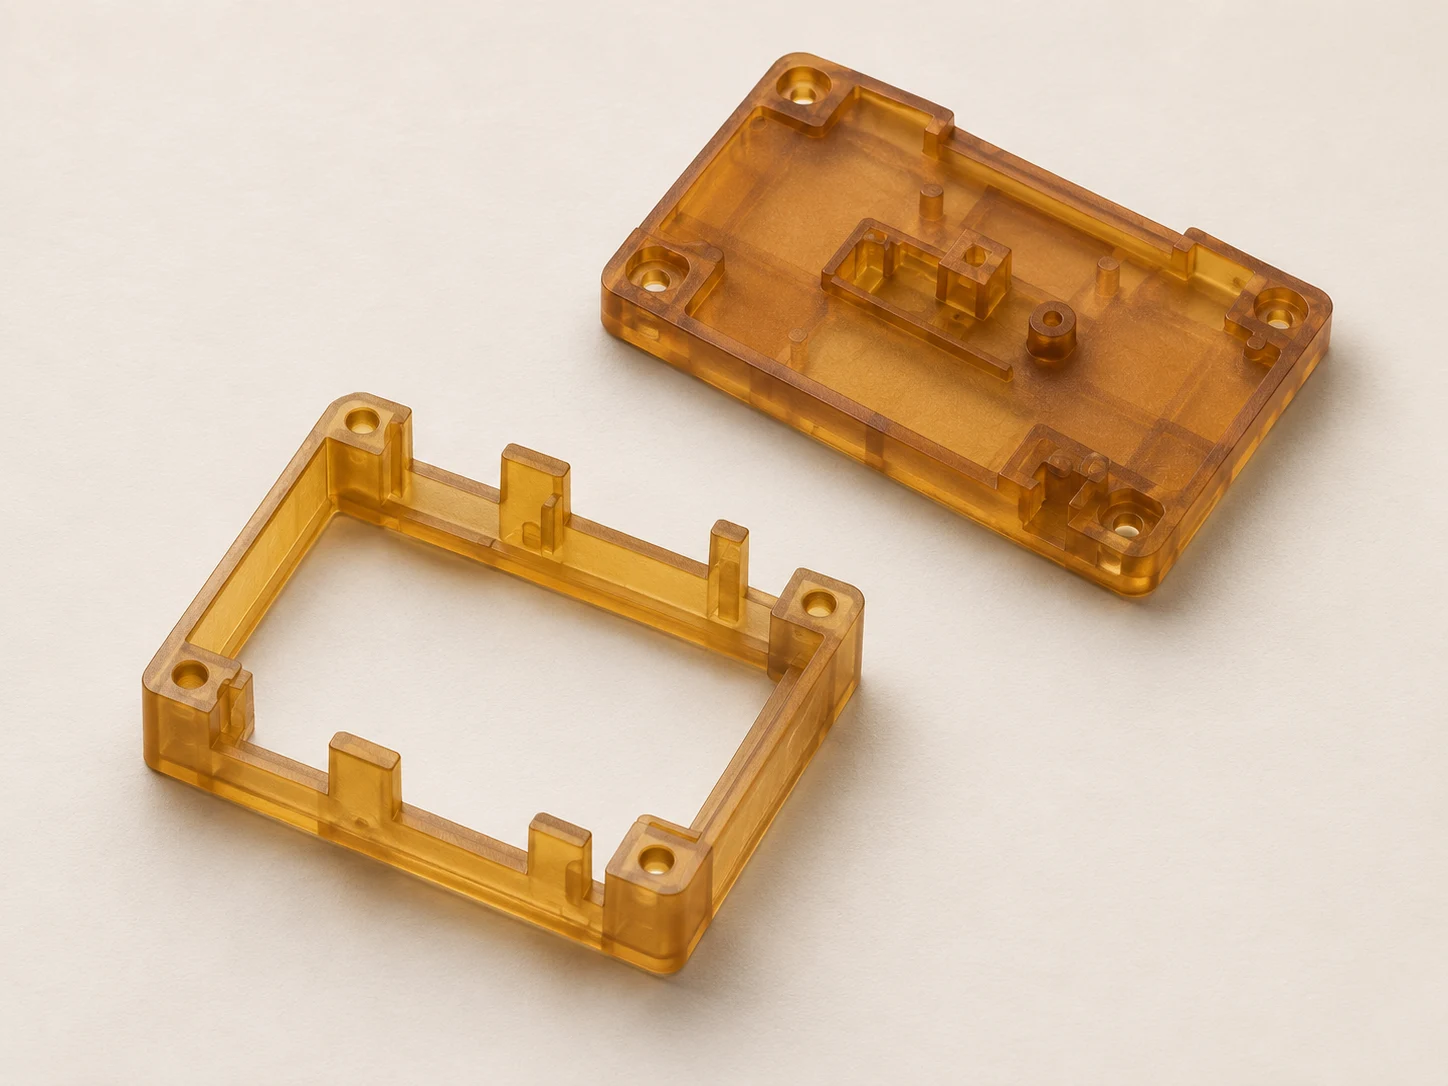
PEI is polyetherimide, an amorphous high-performance thermoplastic. ULTEM is SABIC’s PEI resin brand. Its combination of thermal resistance, stiffness, electrical insulation and dimensional stability supports equipment parts with several functional demands.
Unfilled, glass-reinforced and healthcare formulations have different properties and records. Review chemical exposure, stress, temperature and duration together. SABIC describes ULTEM HU applications in surgical-robot wrist and arm-base components; these uses require appropriate healthcare grades and device validation, with documentation specific to the selected grade and device.

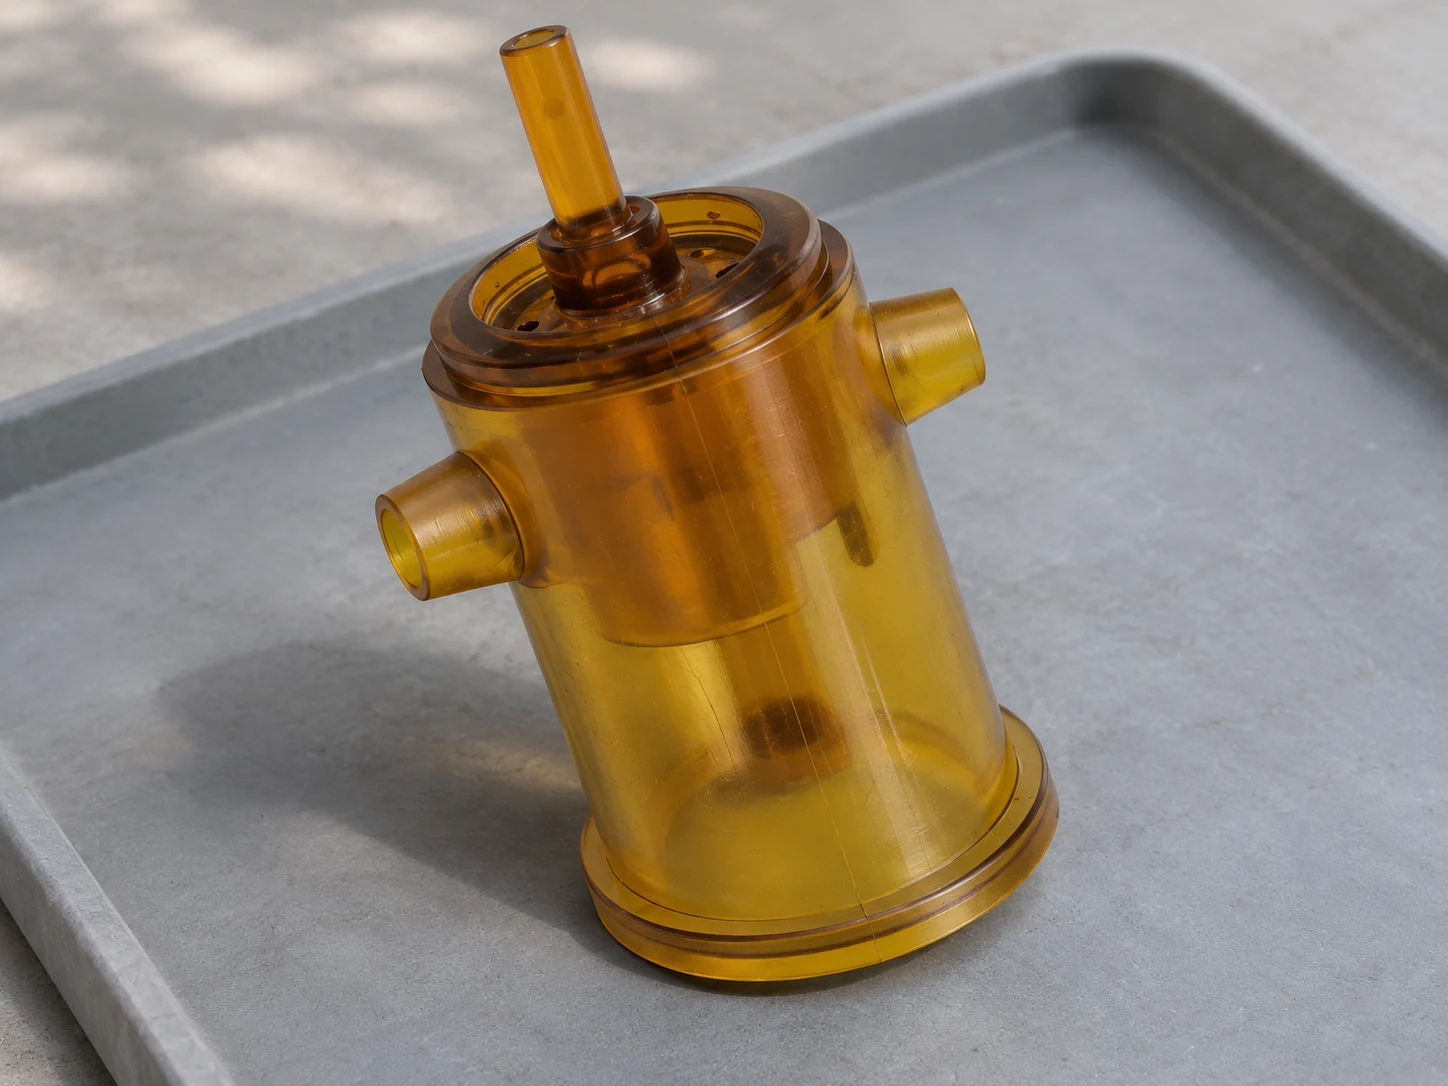
Ported PEI housings bring several connection features into one structure. Define fits, location and assembly acceptance around media, temperature and loading requirements, then confirm function on actual samples.

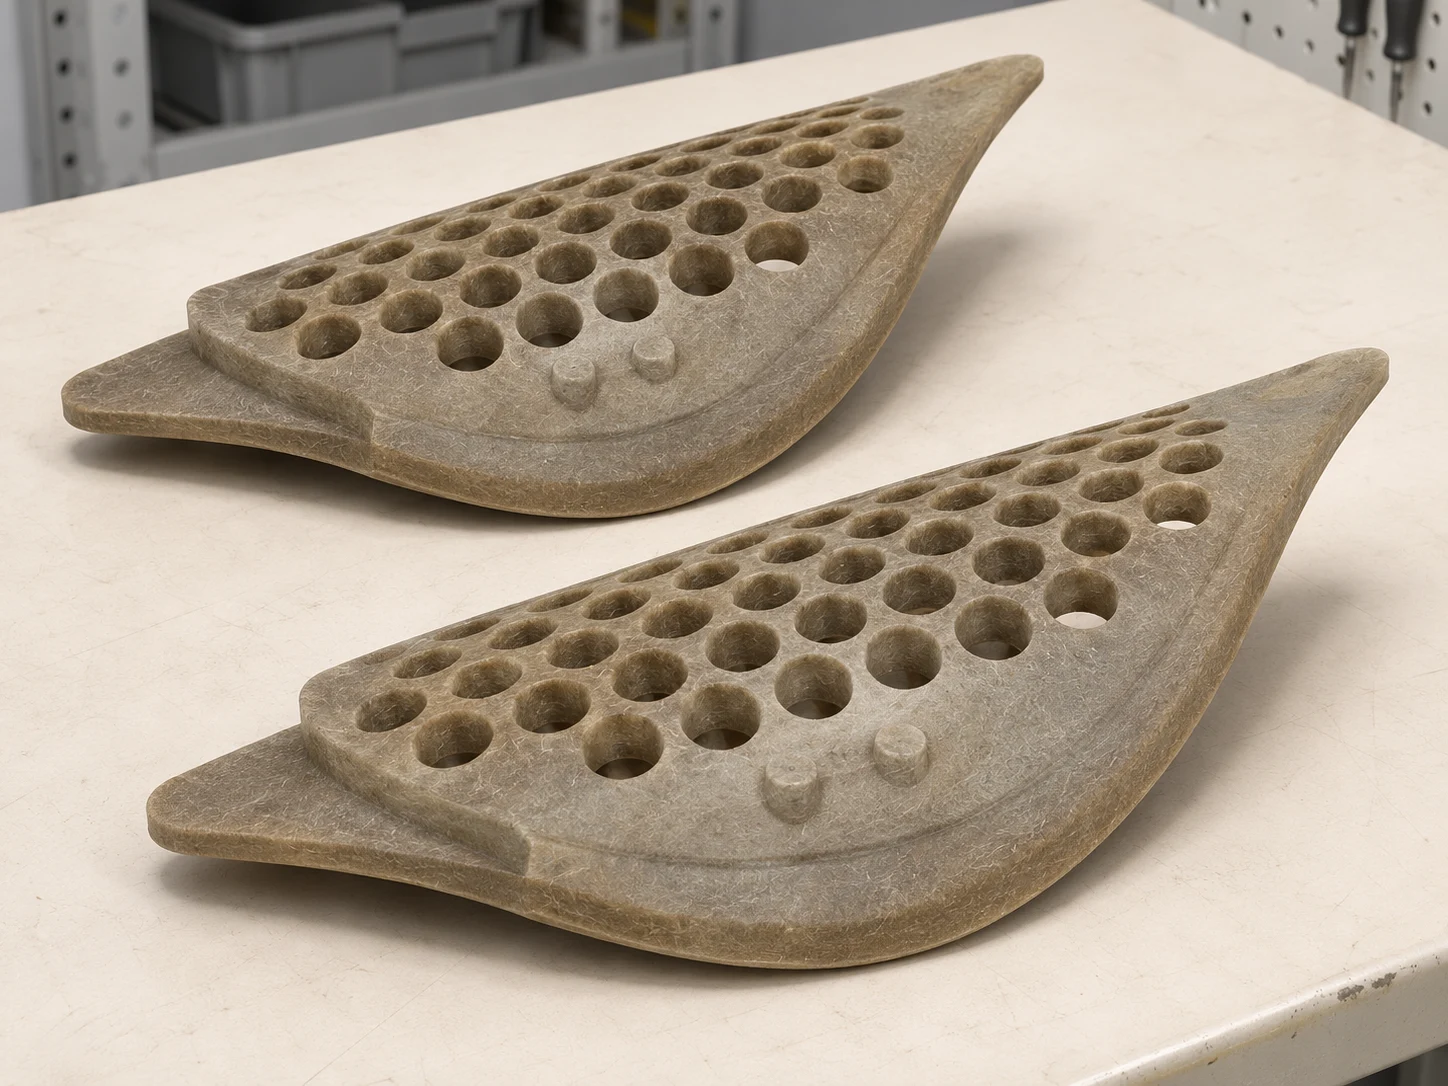
Ribbed housings combine mounting bosses and multiple interfaces within an equipment structure. Review walls, support and assembly space together; where insulation is required, test the selected grade and actual geometry.
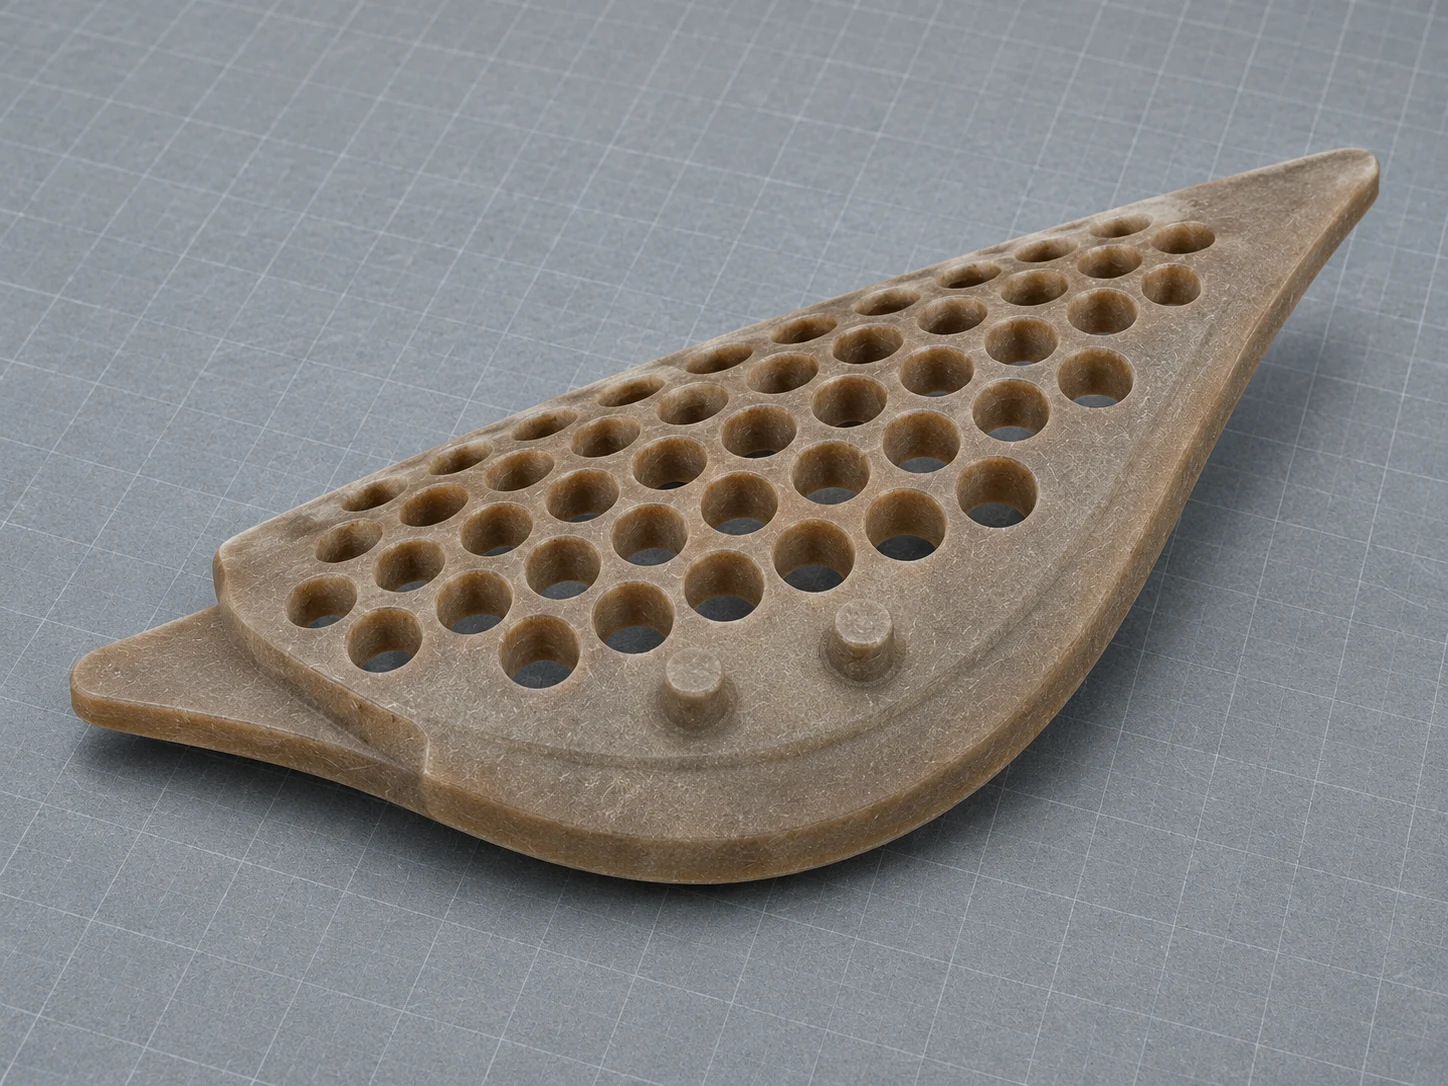
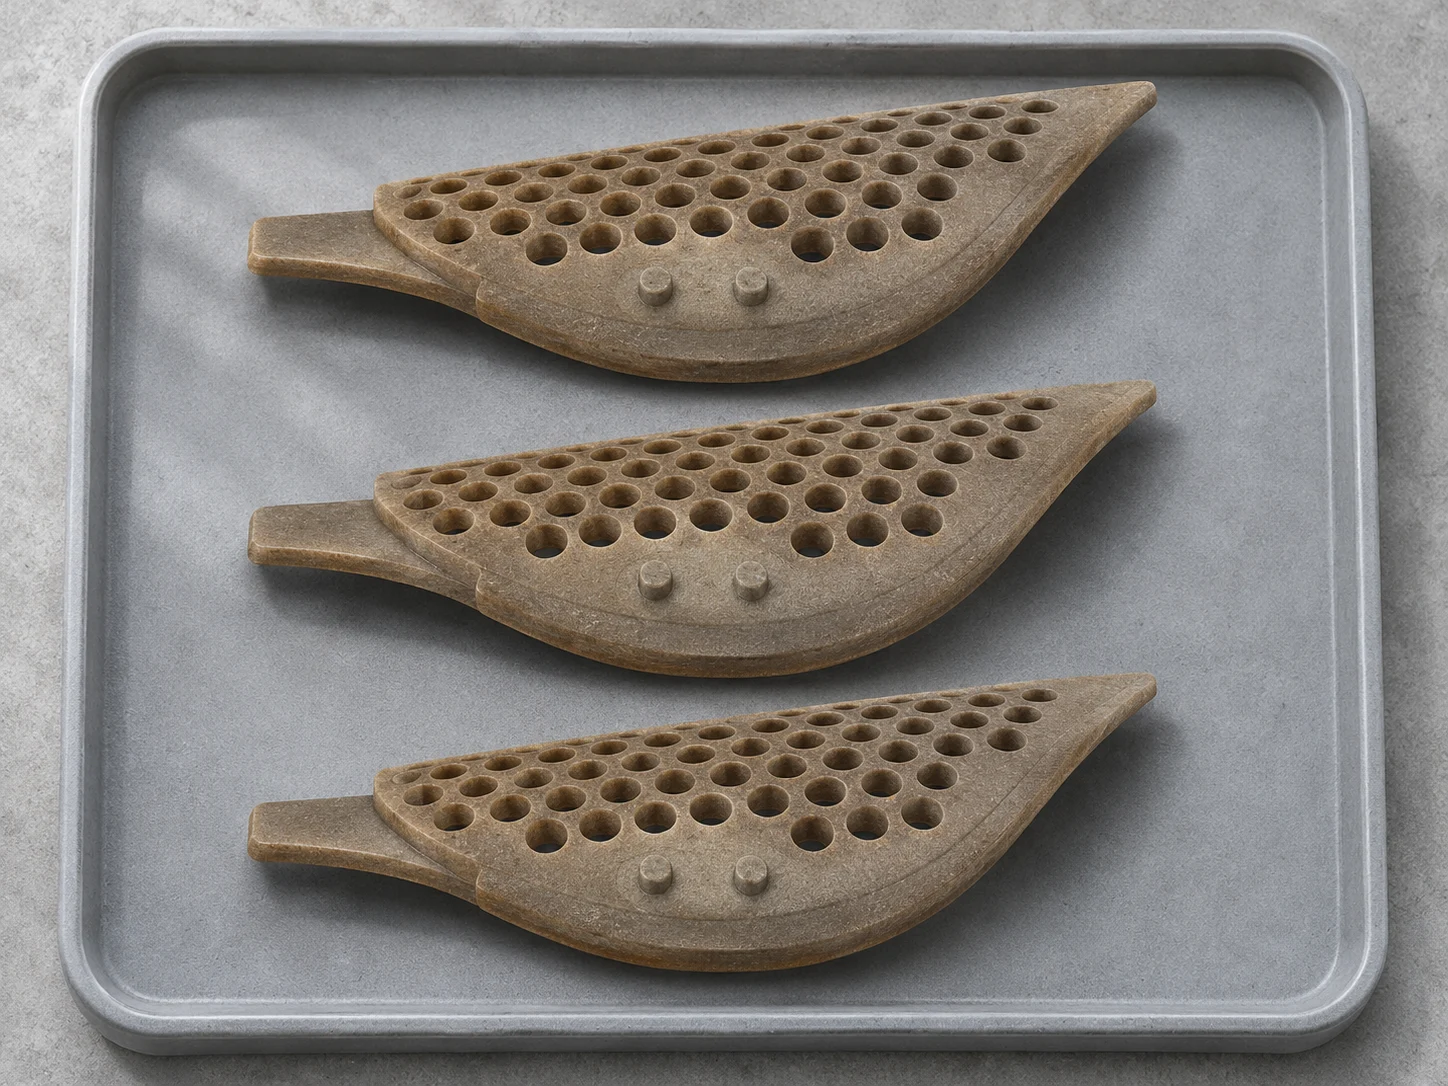
Glass-reinforced PEI can be used for aerospace structural components. Review fiber orientation, local geometry and service loads, then validate samples against the specified grade, material documentation and project requirements.
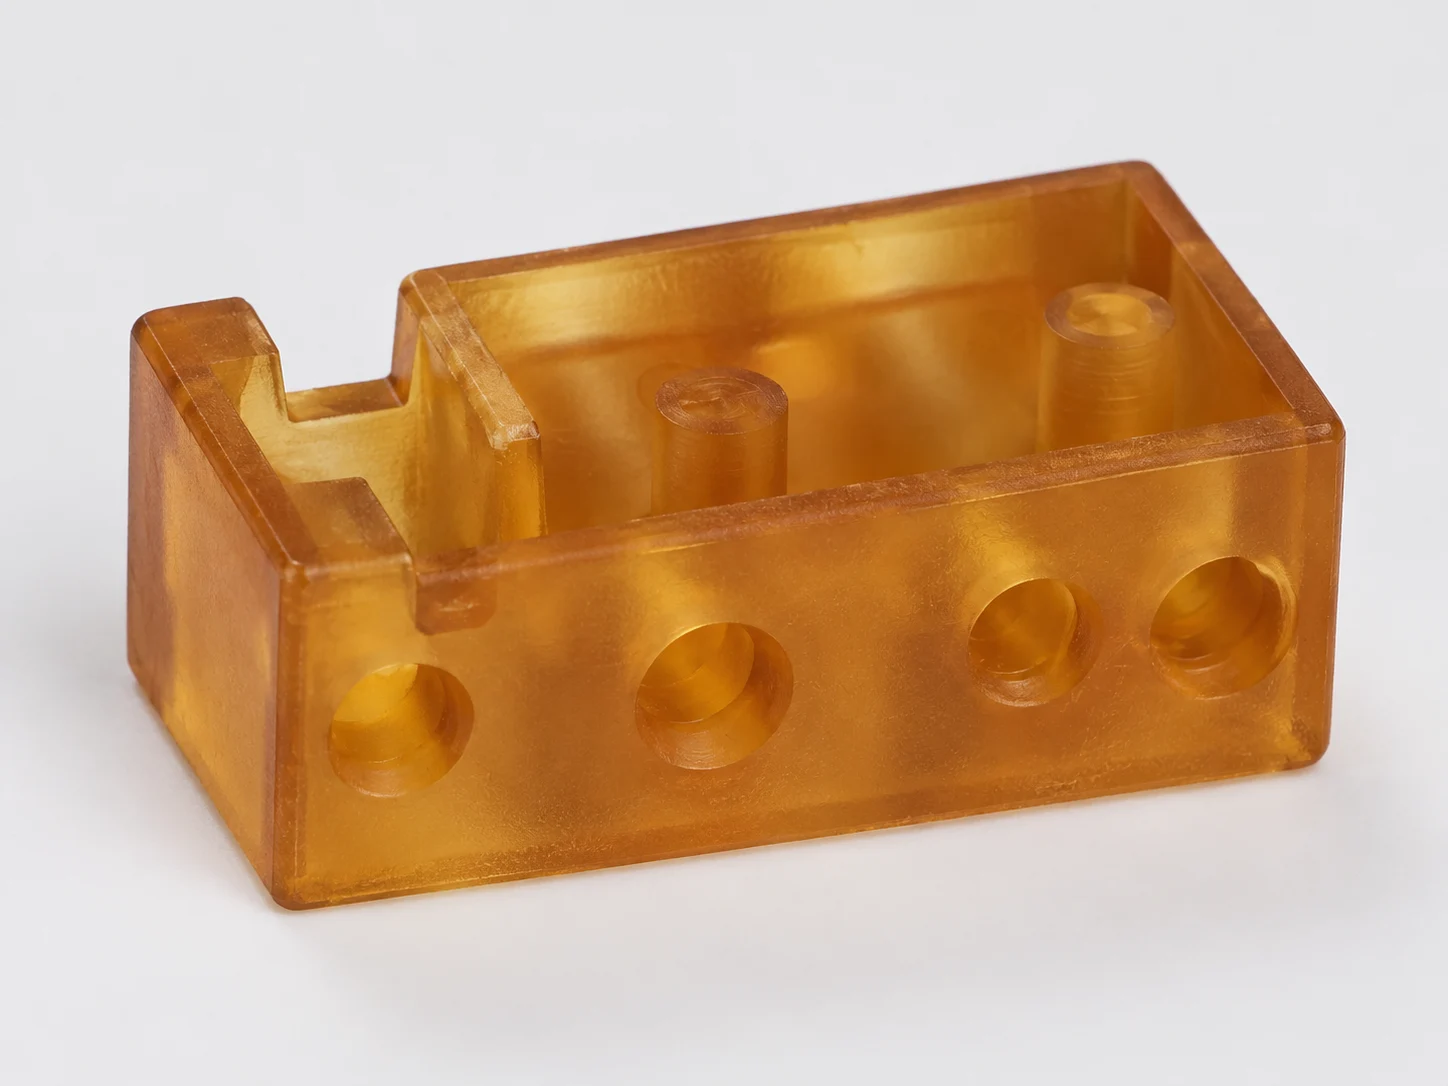
Review openings, internal supports and mounts against neighboring components. Mark fits, load points and measurement datums on the drawing and check assembly on molded PEI samples.
Consider PEI where equipment parts need heat resistance, insulation, stiffness and stable fit together. Compare specific grades and operating conditions rather than using one maximum property value as part validation.
High-temperature processing, drying, tooling and validation all affect cost. For loaded chemical exposure, changing geometry or low quantities, compare material, molding and machining routes before committing to tooling.
PEI INJECTION MOLDING FAQ
Common questions about grades, molding, insulation and project validation.
PEI names the polymer polyetherimide; ULTEM is SABIC’s PEI resin brand, covering multiple unfilled, reinforced and specialty formulations. Specify the exact grade and color for procurement, processing and acceptance rather than the brand alone.
SABIC’s ULTEM 1000 injection guidance lists a 350–410°C melt range. The listed 192°C is ISO HDT under 1.8 MPa for the specified specimen. Set the service temperature separately for the part’s load, exposure and duration.
Moisture and contamination affect high-temperature molding and surface condition. The current Europe-region 1000 table gives injection guidance of 150°C for 4–6 hours with maximum moisture of 0.02%. Equipment, shot size, geometry or another grade may need adjustments; do not mix in extrusion conditions from the same table.
Select for stiffness, load, insulation, color, flow and fit. Reinforcement changes directional and shrinkage behavior, requiring grade-specific data and samples. Unreinforced 1000 values do not represent every glass-filled or healthcare formulation.
Provide critical interfaces, datums and measurement conditions. Review geometry, grade and flow orientation when planning tooling compensation, then set tolerances from tool trials and approved samples.
Select the PEI grade and documentation for the required contact classification, media, temperature and cleaning or sterilization cycles. Verify any biocompatibility, implant or regulatory requirements at the finished-device level.
No. Certain chlorinated solvents, strong alkalis and concentrated acids can cause cracking or crazing under load. Check compatibility for the exact grade, concentration, temperature, contact duration and stress, using relevant tests on actual parts.
Share drawings, quantity and thermal, insulating or cleaning requirements. Our team will review the material and manufacturing route and prepare a quote.
Get a PEI Molding Quote