01
Sampling & Assembly Validation
Review fastening, fit and local loading with molded samples. Define the inspection state before accepting dimensions, then plan functional checks for the required temperature, humidity and cycles.
Built for production.
Take your design from tooling to repeat production of custom plastic parts.
Manufacturing Capabilities
Plastic Injection MoldingCustom plastic parts for production Tooling & Design SupportPrepare your part design for tooling High-Volume ProductionPlan repeat runs around your delivery needsMaterials & Finishes
Made for smaller runs.
Produce resin parts with silicone molds for design validation and small batches.
Small-Batch Capabilities
Vacuum CastingResin parts made with silicone moldsLow-Volume ProductionFrom trial parts to small-batch deliveryAppearance & Fit ChecksPrepare multiple parts for product checksMaterials & Finishes
Other Services
Machining, printing, and supporting services for specific part needs.
Materials & Finishes
Explore material performance and appearance options separately.
Explore Materials & Finishes
Injection Molding Materials
Choose molding materials for strength, heat resistance and appearance.
Manufacturing Knowledge
Find articles, answers, and case studies to help prepare your project.
Start with your part requirements.
Contact PlasticHubs for help with quotes, files, delivery, and orders.
Files, Orders & Delivery
Industries
Explore manufacturing options for your product application.
Start with your manufacturing needs
From tooling to production of plastic parts.
Small batches of resin parts made with silicone molds.
Start with your design, material, and quantity.
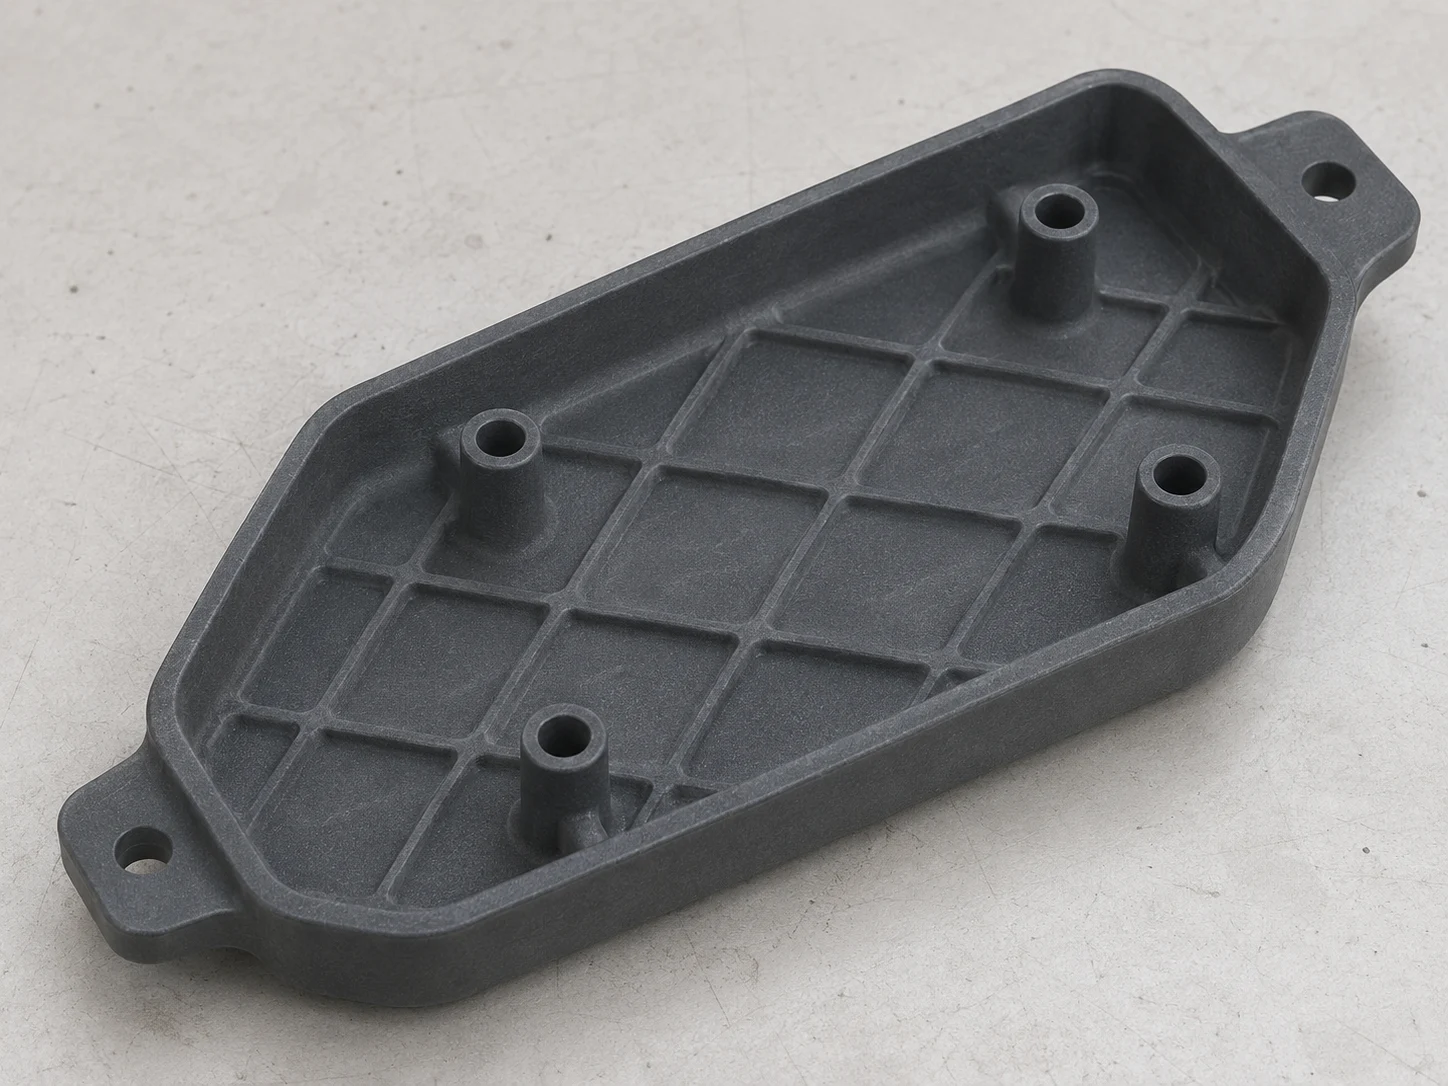
Plan PA66 molded components around operating temperature, fastening loads and repeated assembly. Connect the grade, drying, fiber direction and conditioned fit requirements with tooling, samples and production acceptance.
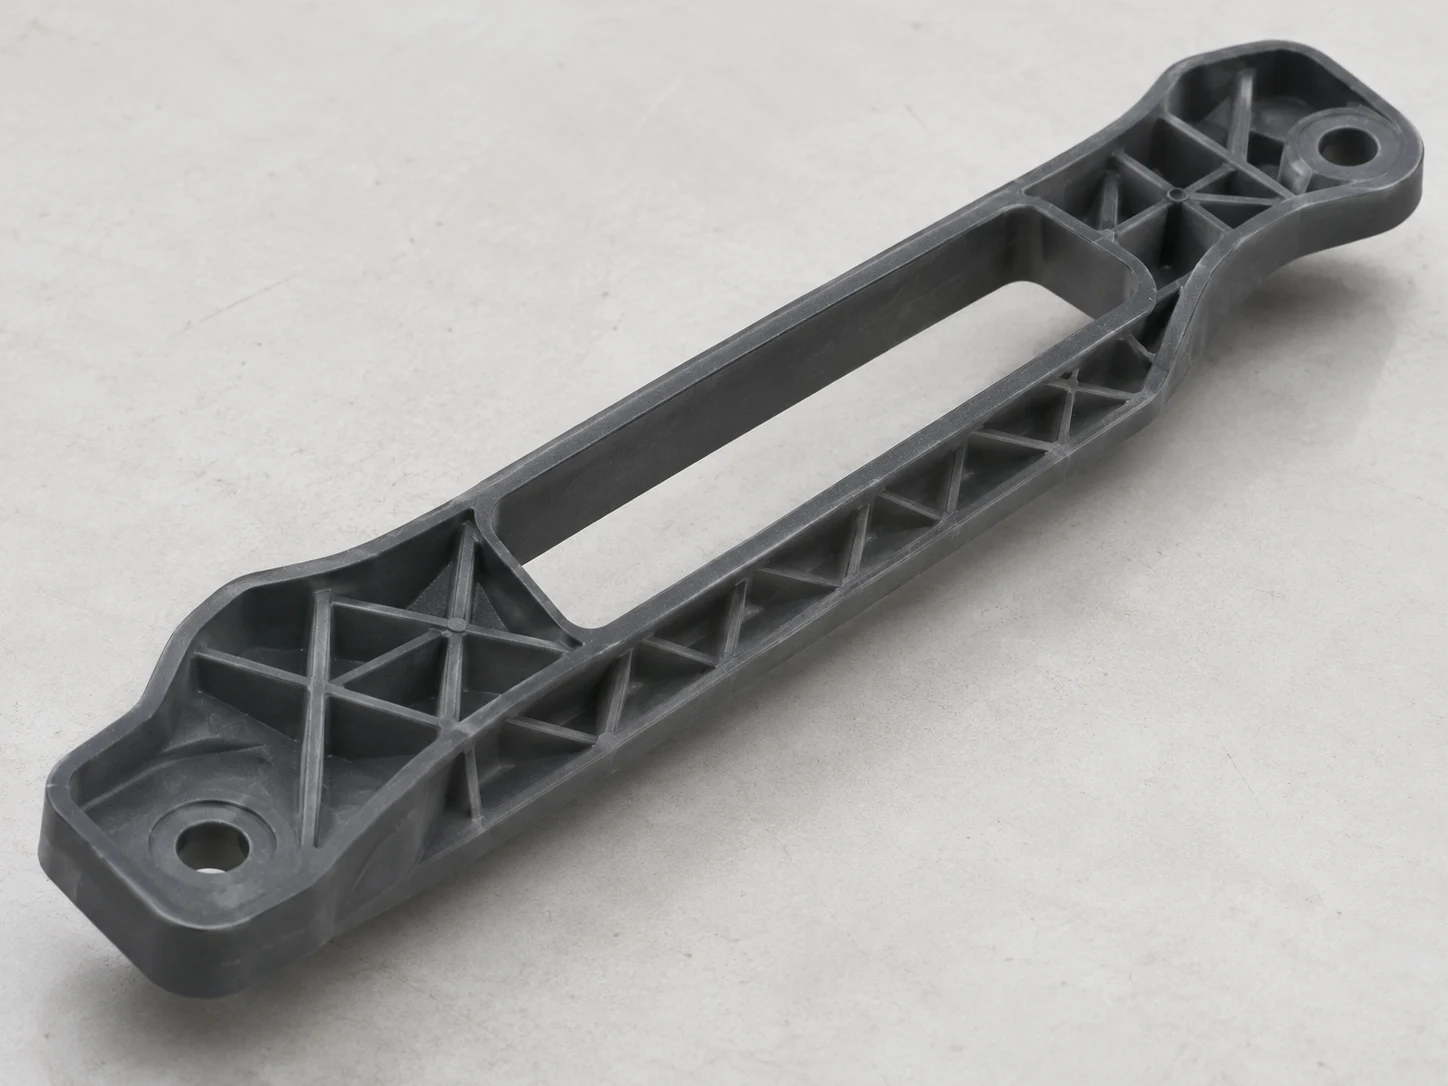
Describe sustained and peak temperatures, load duration, fastening method and service humidity. For critical connections, specify torque, fit or cycle targets so grade selection and sample acceptance reflect the operating conditions.
Discuss your project ↗Review fastening, fit and local loading with molded samples. Define the inspection state before accepting dimensions, then plan functional checks for the required temperature, humidity and cycles.

Create comparable production conditions from resin lots and drying records to mold temperature, cooling and cavity dimensions. Connect approved samples with storage, conditioning and inspection methods.
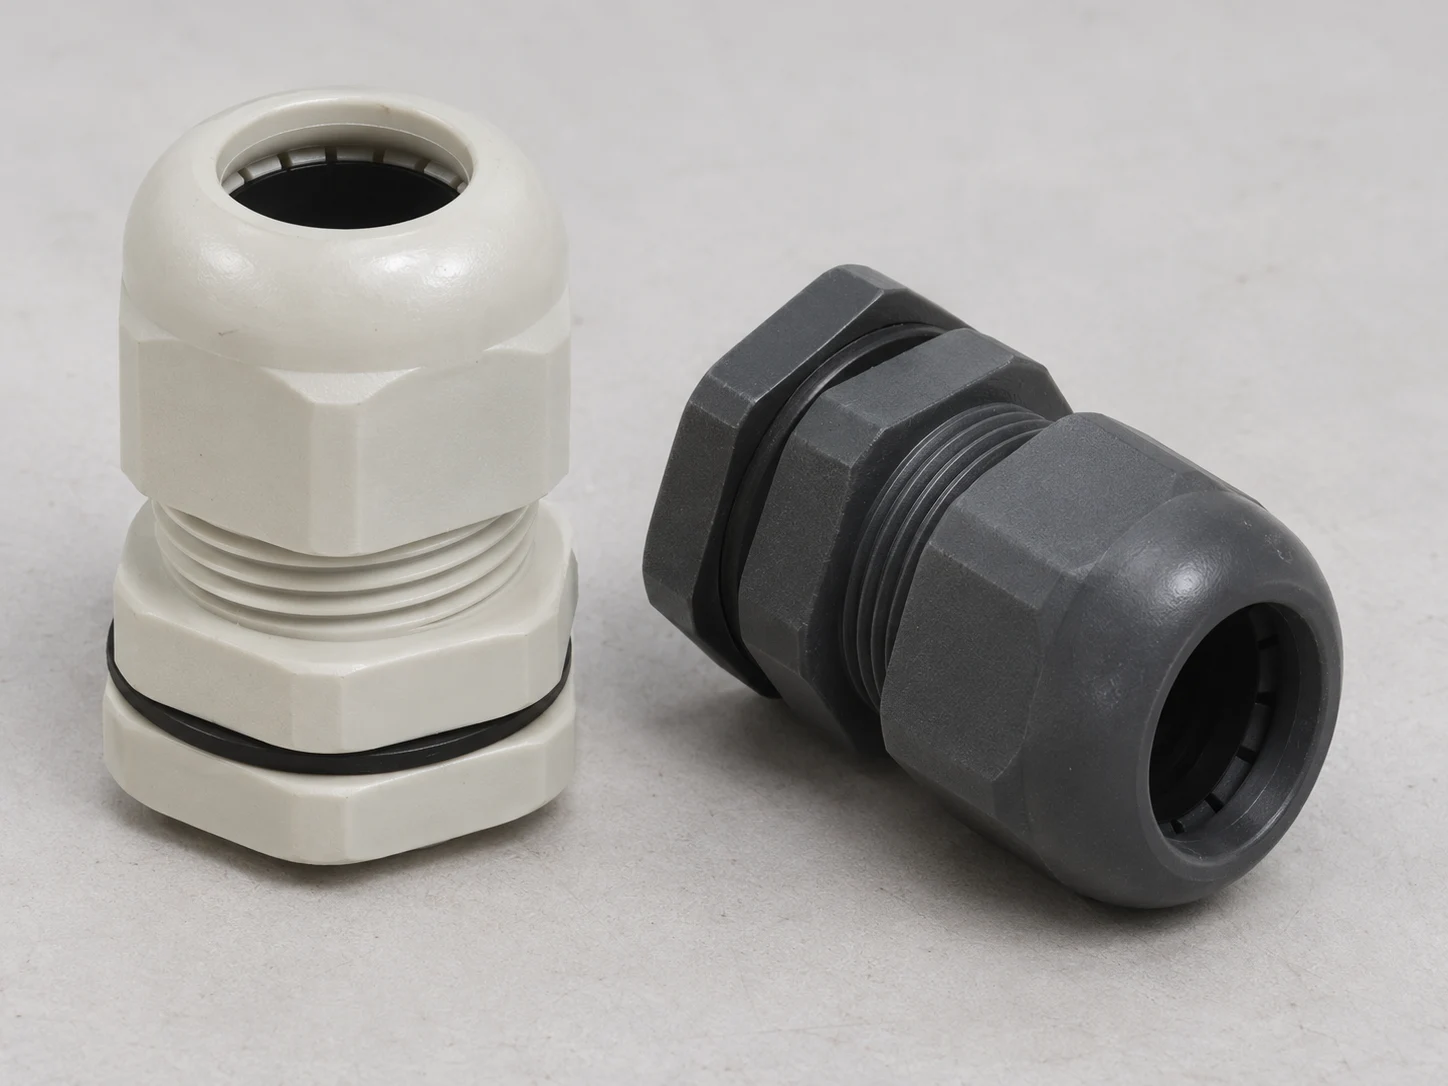
Compare unfilled, glass-filled and modified PA66 for thermal loading, stiffness, toughness and exposure. Specify the full grade, filler content, stabilizers and color.
Share your drawings, quantity, temperature and fastening or assembly requirements.
| Item | Project review |
|---|---|
| Material & service conditions | Select the grade for thermal loading, moisture, reinforcement and documentation |
| Tooling & cavities | Review gates, cooling and flow direction against the load path |
| Dimensions & assembly | Agree on datums, fit and measurement conditions before or after conditioning |
| Sampling & production | Connect tool trials, functional validation and batch acceptance |
| Surface & marking | Review texture, color, fiber read-through and marking compatibility |

Set drying, moisture and processing limits for the selected PA66 grade. When troubleshooting splay or performance changes, check moisture, contamination and residence history together.
Review gates and weld lines against loaded areas. Fiber orientation affects stiffness, shrinkage and warpage in glass-filled grades, so mounting faces and holes must be checked with the flow plan.
Use gradual transitions and coring at heavy sections, with balanced cooling and ejection support. Crystallization shrinkage and subsequent moisture uptake can affect dimensions; specify measurement timing and conditioning state.
Review local stress, torque and pull-out loads at screws, inserts and clips. Check creep, fatigue and repeat assembly at the expected temperature and humidity.
Separate tool finish, resin color and marking requirements for visible areas, grip zones and service exposure. Confirm reinforcement-related appearance with the selected grade and samples.
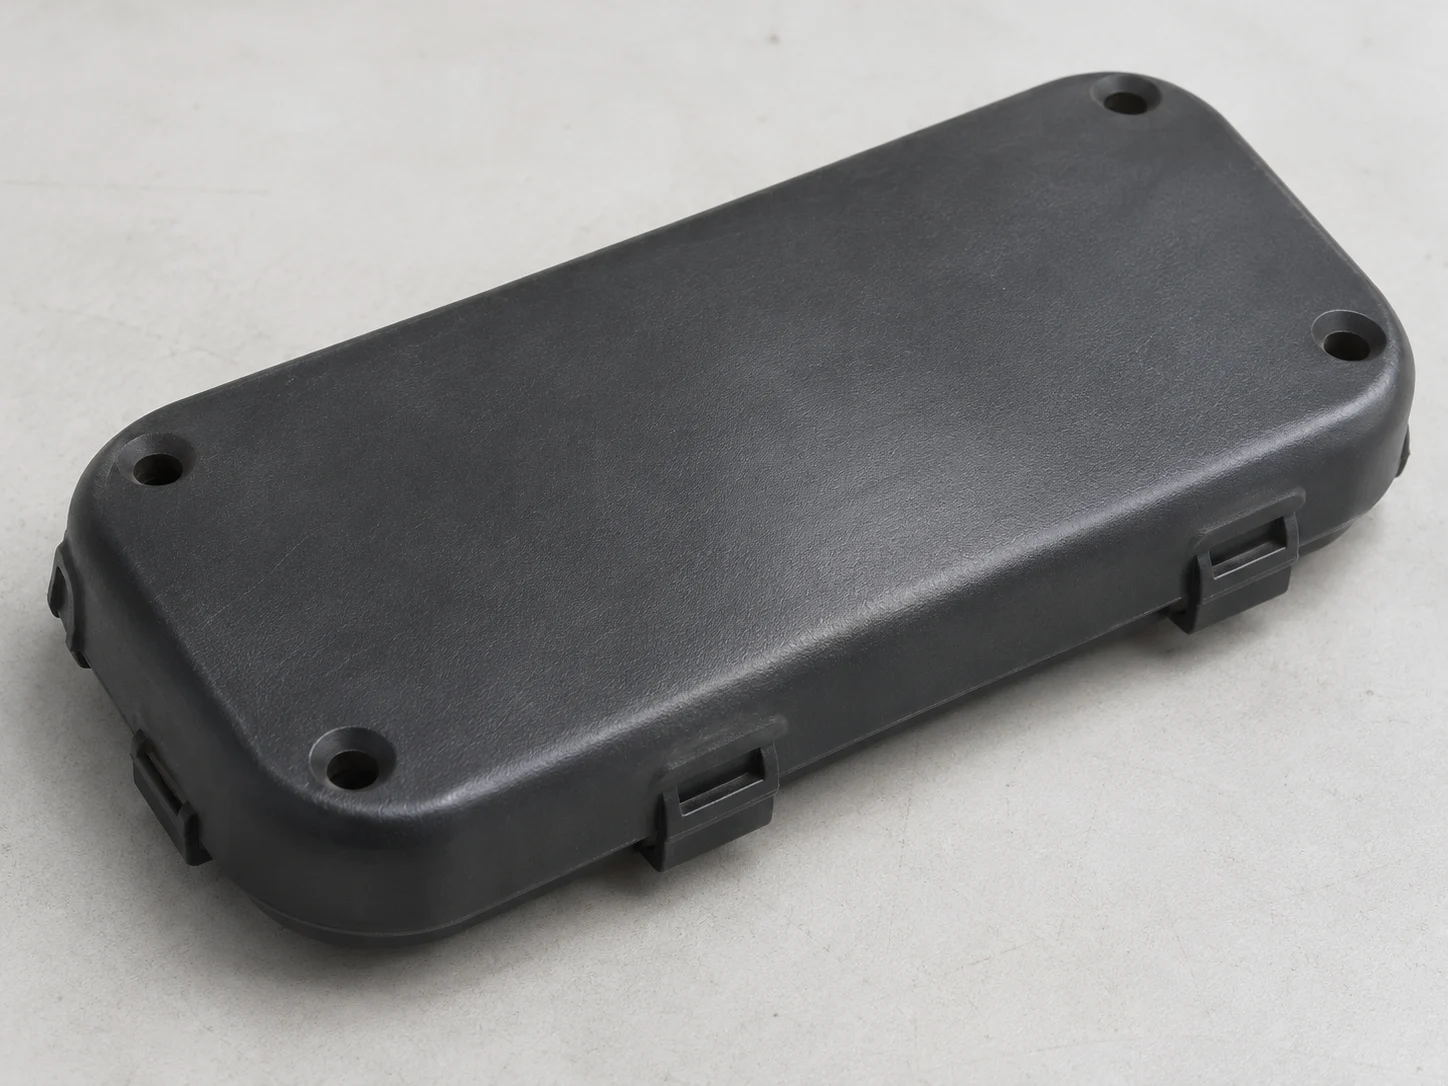
Plan a smooth surface through the tool finish without equating tool polish with part gloss. Glass fiber, color and processing affect the PA66 surface; use approved samples for acceptance.
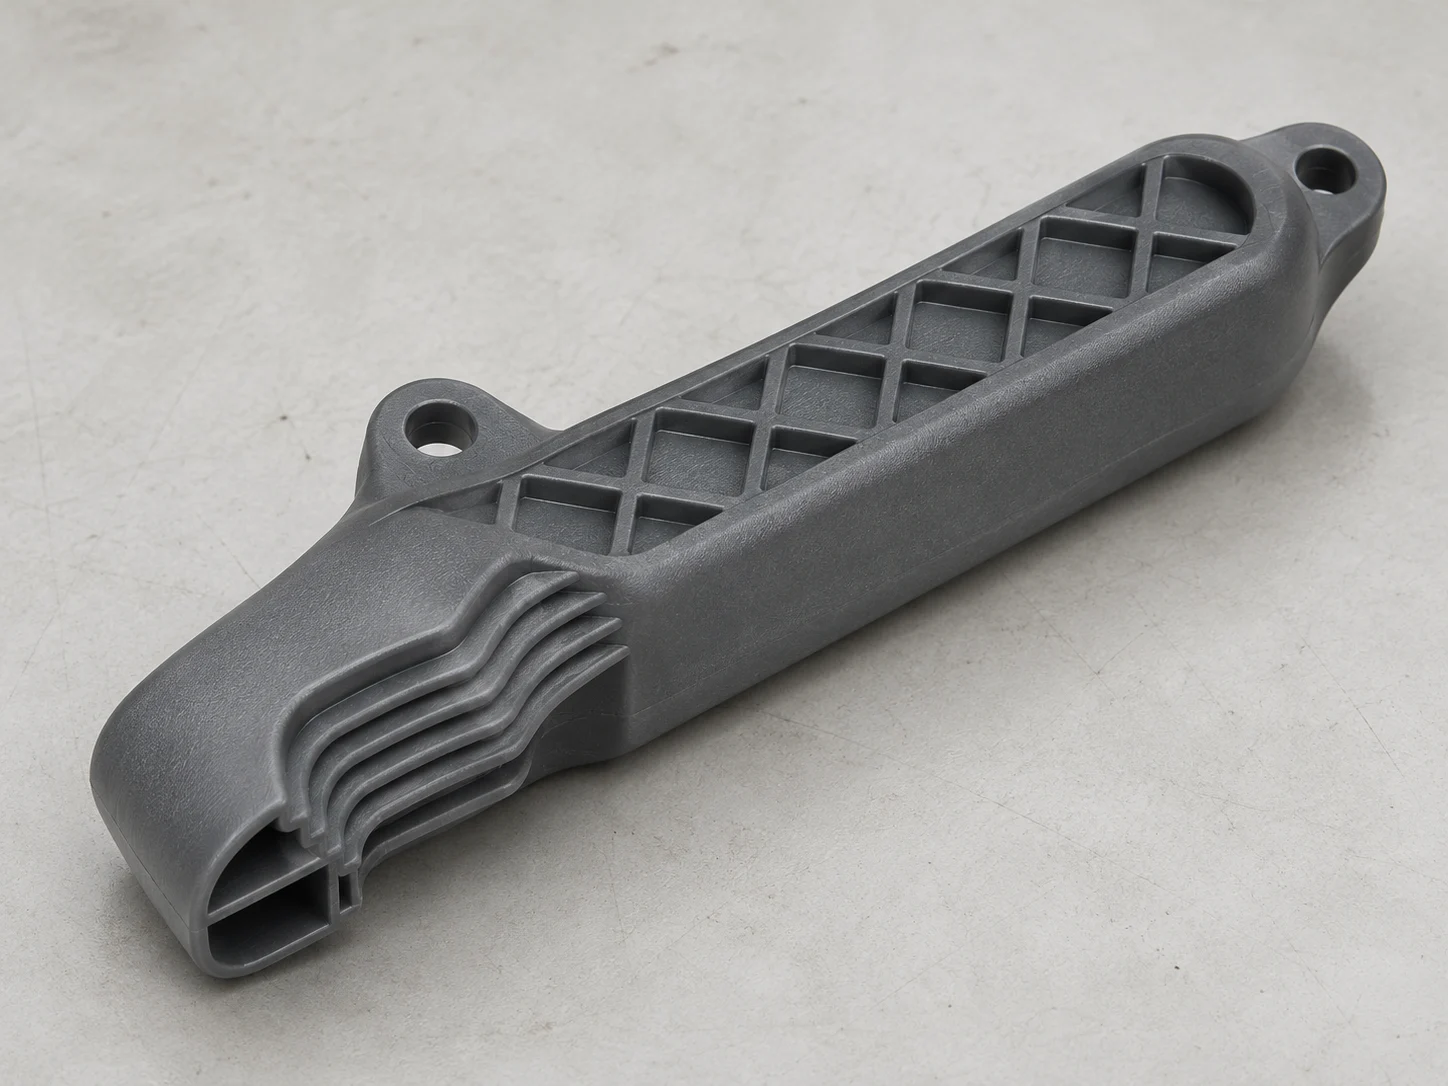
Use texture for knob grip or housing appearance while reviewing demolding, cleaning and wear contacts. Agree separately on weld lines and fiber read-through within specified visible areas.

Review color together with the PA66 grade, reinforcement level and stabilizers. Check documentation and performance when changing color; different formulations are not simply interchangeable colors.

Select the ink and surface preparation for the PA66 grade, filler and conditioning state. Test marking adhesion, rub resistance and cleaning durability on molded samples.
Check dimensions, appearance and function separately, recording conditioning and measurement conditions for critical dimensions. For fastening or load-bearing areas, validate torque, pull-out, cycles or thermal loading within the agreed scope.
The CAMPUS datasheet for BASF Ultramid A3K supplies the typical data and processing recommendations below. Paired results are listed dry first and conditioned second. Use separate data when evaluating a glass-filled grade.
| Property | Typical value | Method / condition |
|---|---|---|
| Density | 1,130 kg/m³ | ISO 1183 |
| Tensile modulus, dry / conditioned | 3,000 / 1,100 MPa | ISO 527 |
| Yield stress, dry / conditioned | 85 / 50 MPa | ISO 527 |
| Notched Charpy impact, dry / conditioned | 5 / 20 kJ/m² | ISO 179/1eA; +23°C |
| Molding shrinkage, parallel | 1.5% | ISO 294-4, 2577 |
| Molding shrinkage, normal | 1.8% | ISO 294-4, 2577 |
| Property | Typical value | Method / conditions |
|---|---|---|
| Melting temperature | 260°C | ISO 11357-1/-3; 10°C/min |
| Heat deflection temperature | 75°C | ISO 75-1/-2; 1.80 MPa |
| Drying | 80°C; 4 h | Supplier processing recommendation |
| Maximum allowed water content | 0.15% | Supplier processing recommendation; before molding |
| Melt-processing temperature | 280–300°C | Supplier injection-molding recommendation range |
| Mold temperature | 60–80°C | Supplier injection-molding recommendation range |
| Water absorption, published value | 8.5% | Sim. to ISO 62; exposure duration not shown on the page |
Use the dry and conditioned values for their respective measurement states. Keep melting point, HDT and the intended continuous-use temperature distinct. Use the injection recommendations for tool trials and the specimen-production conditions to interpret the test data.
Reference grade: BASF Ultramid A3K, CAMPUS datasheet. Read on 2026-10-20; no document revision date was displayed.
Review temperature, loads and humidity together, identifying the required stabilizers, reinforcement and color.
Connect tooling, trials and acceptance requirements through our group manufacturing resources, reducing information gaps between project stages.
Define sample checks around torque, fit and repeated assembly, matching load directions to local features.
Keep grades, moisture records, conditioning and measurement conditions comparable between sampling and subsequent production.

Nylon 66, written as PA66 or PA6/6, is a semi-crystalline polyamide engineering thermoplastic. It can serve molded components requiring stiffness, wear or thermal-load performance, with behavior determined by the grade and operating conditions.
PA66 and PA6 are different materials. Unfilled, glass-filled, heat-stabilized and other modified PA66 grades are not interchangeable on the nylon name alone; moisture, color and formulation affect dimensional and performance review.

Plan stiffness and cooling around ribs, bosses and wall transitions. Review shrinkage, flow and conditioned assembly for mounting faces and loaded areas.
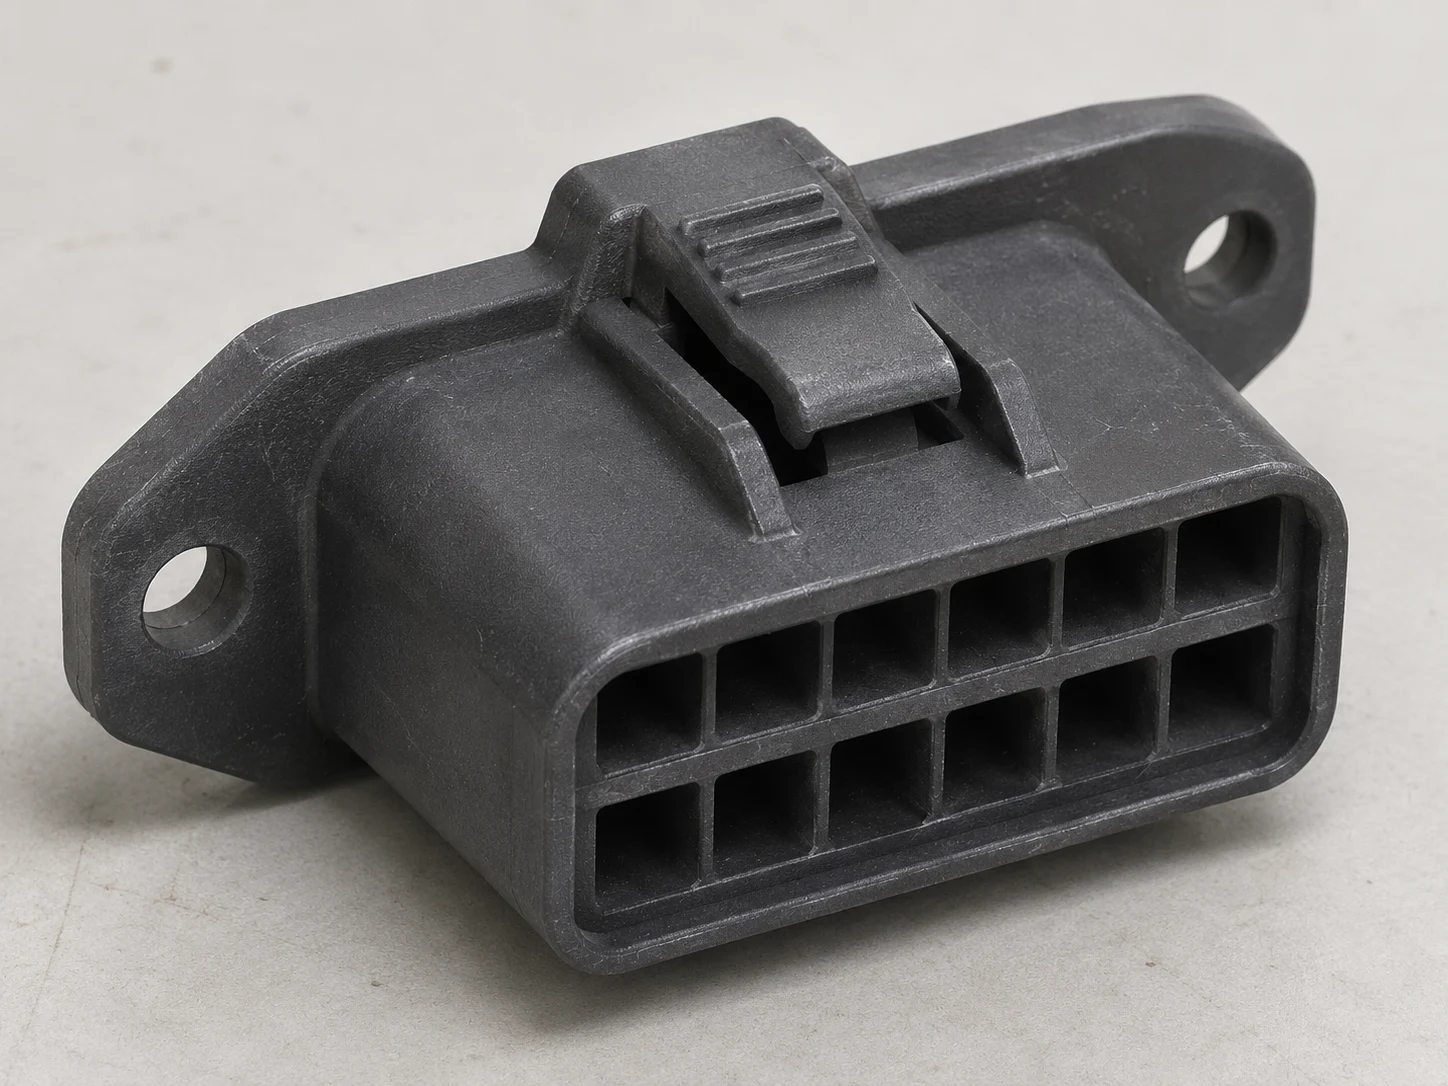
Review PA66 contact chambers, latches and mounting flanges. Connect retention, thermal loads, insulation and dimensional requirements with the selected grade and validation conditions.
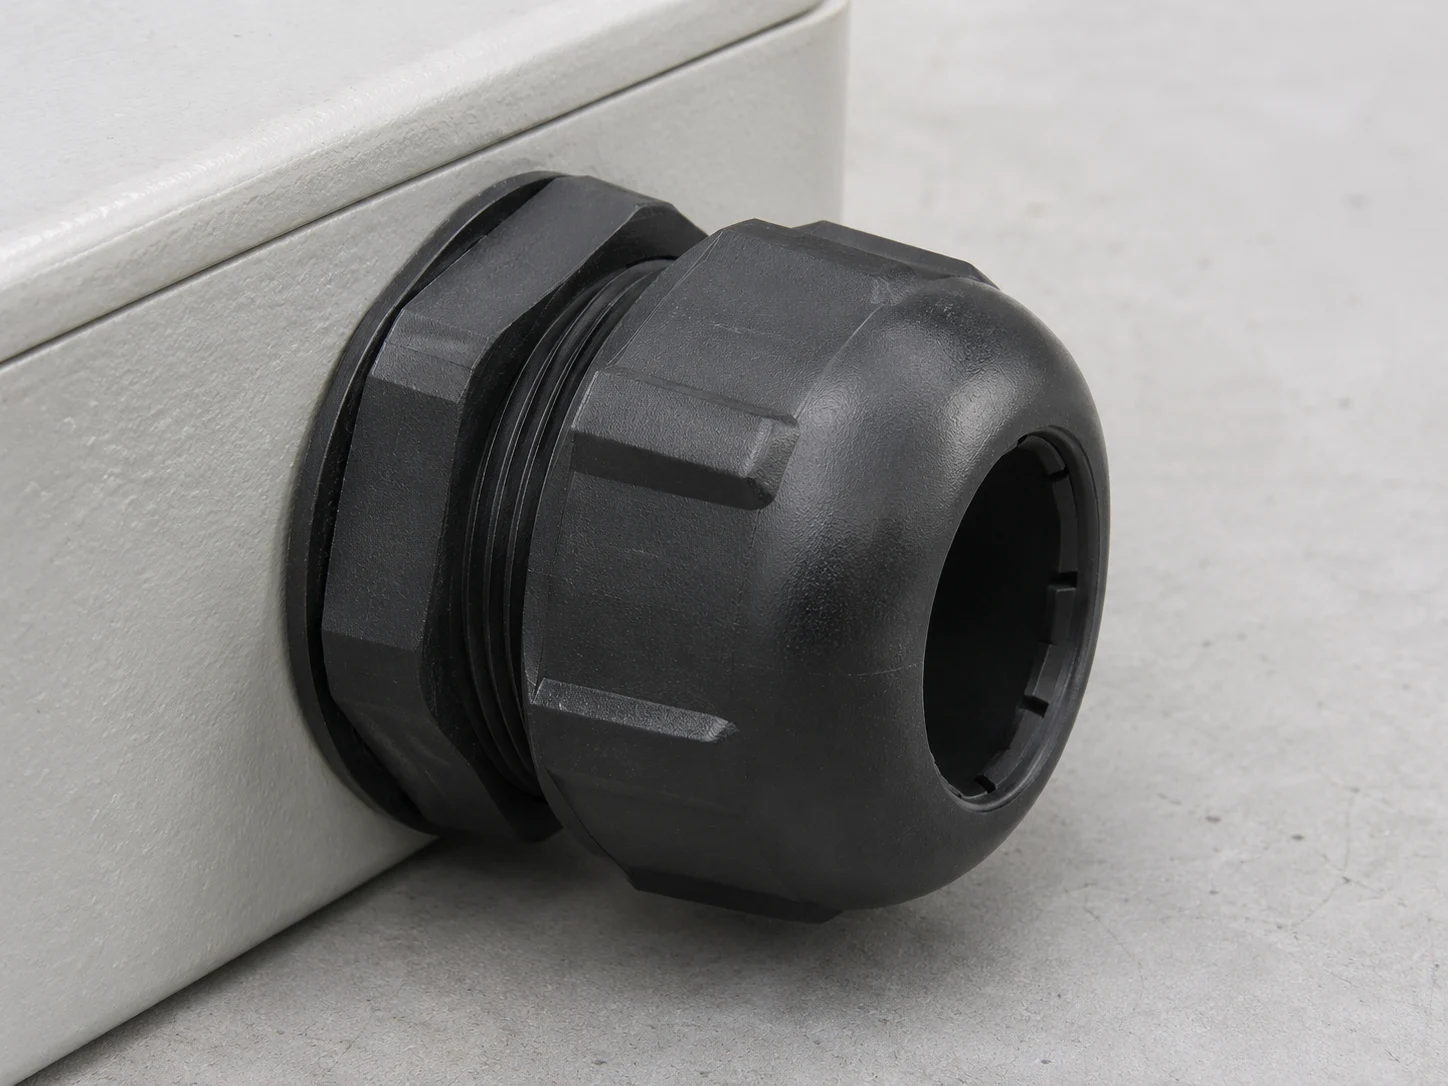
Review threads, retention and mounting interfaces for cable-entry hardware. Sealing or protection ratings require validation of the complete component.
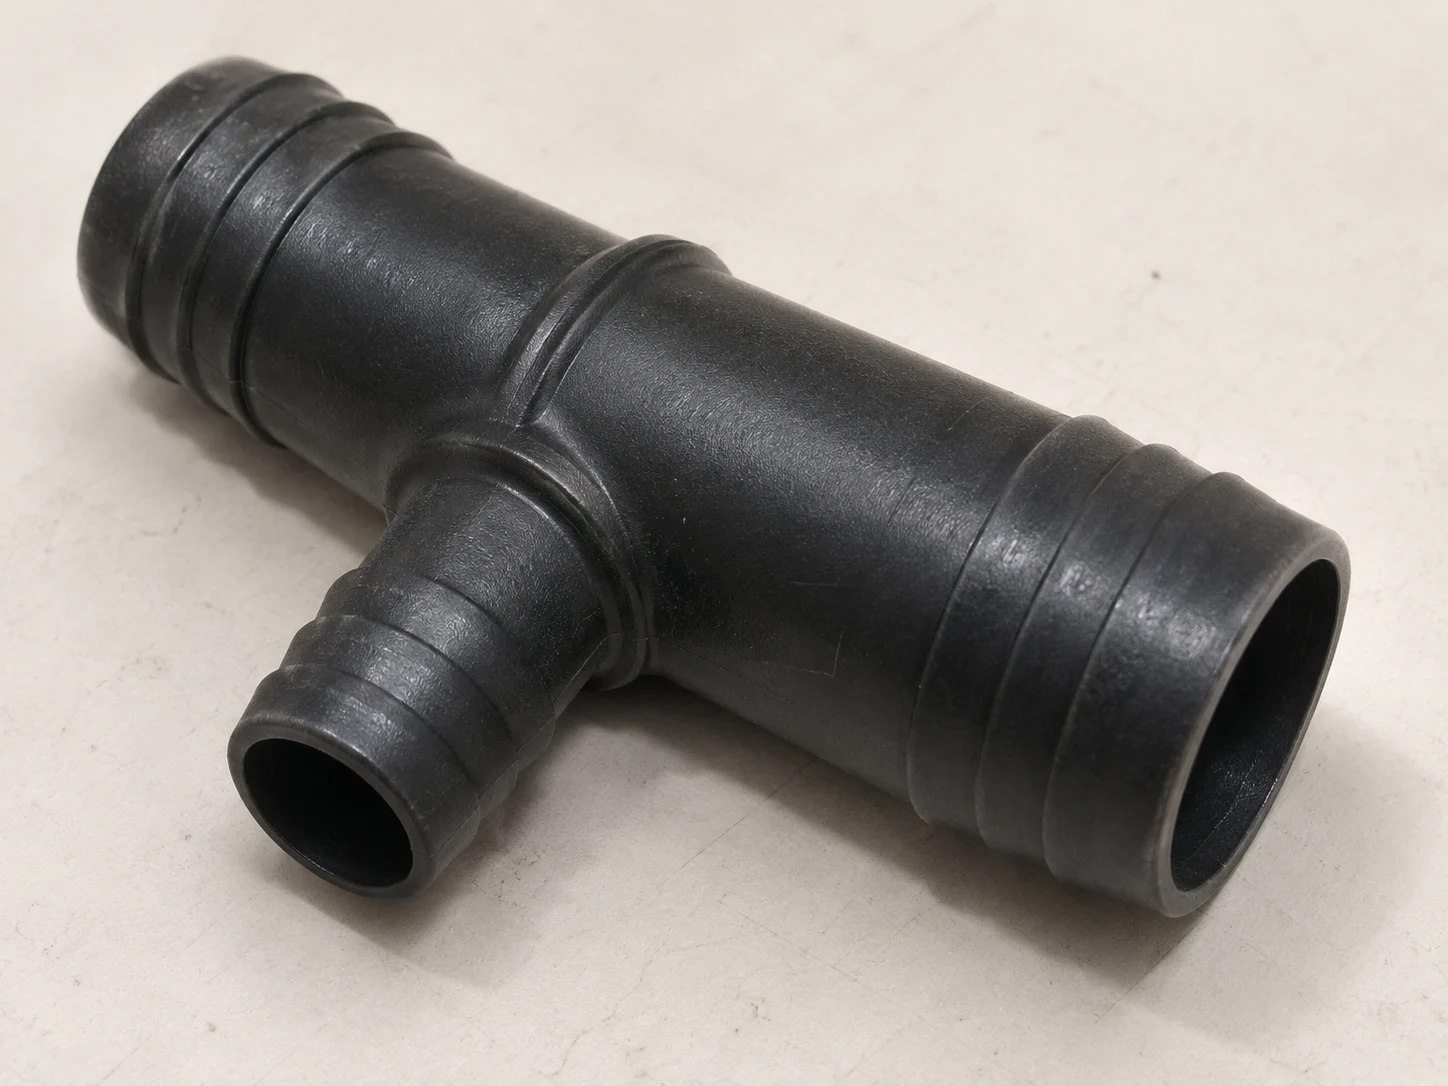
Review interface fit, connection loads, media and temperature. Establish pressure, sealing and durability requirements for the selected grade, design and finished-part tests.
PA66 formulations provide options for load-bearing, fastening or motion components. Molding can integrate bosses, connections and grip features; evaluate tooling, resin and validation effort against lifetime demand.
Compare PA66, PA6 and other candidate grades by conditioned dimensions, retained stiffness, sustained load, chemical exposure and appearance in the intended operating environment.
PA66 INJECTION MOLDING FAQ
PA66 grades, thermal loading, moisture, reinforcement and connection questions.
PA66 and PA6/6 both identify nylon 66; PA6 identifies nylon 6. Their formulations and processing windows differ. Check full grade designations and dry/conditioned data rather than treating similar names as one material.
For BASF Ultramid A3K, the drying guidance is 80°C for 4 hours with maximum allowed water content of 0.15%. Check the selected grade’s instructions and record bag exposure, feeding and hopper conditions.
No. Drying controls moisture before processing; conditioning brings the molded part to an agreed state. Define conditioning, exposure and measurement timing for critical fits and fasteners so tool corrections are not based on temporary dry dimensions.
Along with stiffness and strength, review flow orientation, weld lines, directional shrinkage and fiber read-through. Consider gates, mounting faces and load paths together, then confirm warpage, holes and assembly with samples.
The choice depends on the part. Compare specific PA6 and PA66 grades for retained stiffness, toughness and fit under matched moisture and test conditions. Set sustained operating temperature from the actual load and exposure.
Specify torque, pull-out and repeated-assembly requirements, then review bosses and local walls. Include temperature, humidity and sustained loading in the sample test plan.
Share CAD, drawings, quantity, the full grade or functional targets, including reinforcement, color, temperature/humidity, loads and acceptance state. Tool complexity, resin, cavities, cycle, secondary operations and validation scope all affect quotation.
Share your CAD, material, quantity, and key requirements. Our team will review your project and prepare a quote.
Request a Quote